
Leading China Factory
Mens Knit Polo Shirts Sweaters Wholesale Supplier
Mens knit polo shirts sweaters are produced using soft yarns and advanced knitting techniques to create refined textures and comfortable fits. As a wholesale supplier and manufacturer, we support custom knitwear development including style design, material selection and bulk production. Our process ensures consistent quality, flexible quantities and reliable supply, helping brands build strong polo knit collections for global markets.
- Home
- Custom Men's Sweater
- Polo Sweaters
Custom Men's Sweater
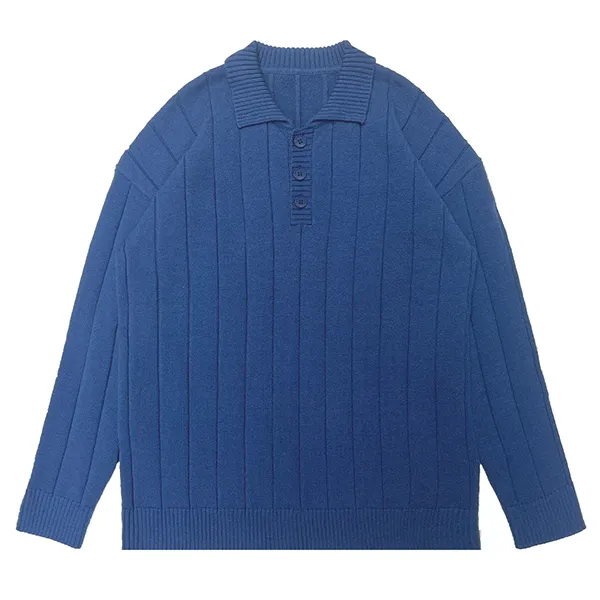
Relaxed Fit Long Sleeve Ribbed Knit Polo Pullover Sweater with Drop Shoulder Button Placket and Ribbed Trim Manufacturer
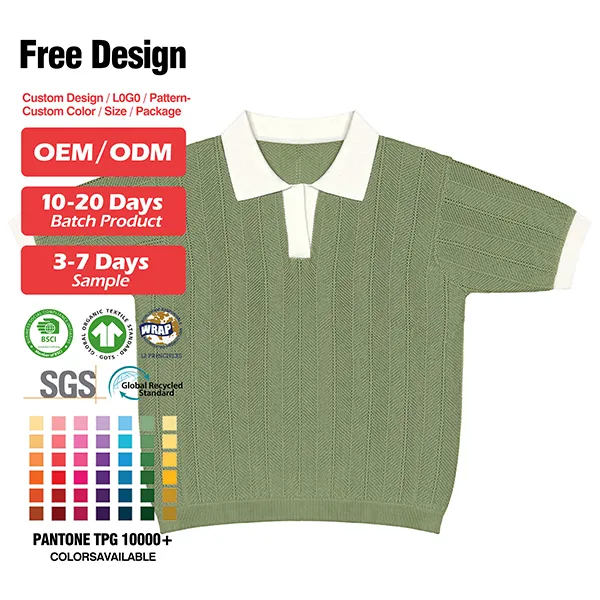
Relaxed Fit Herringbone Textured Short Sleeve Knit Polo with Contrast Collar Placket and Ribbed Trim OEM Manufacturer
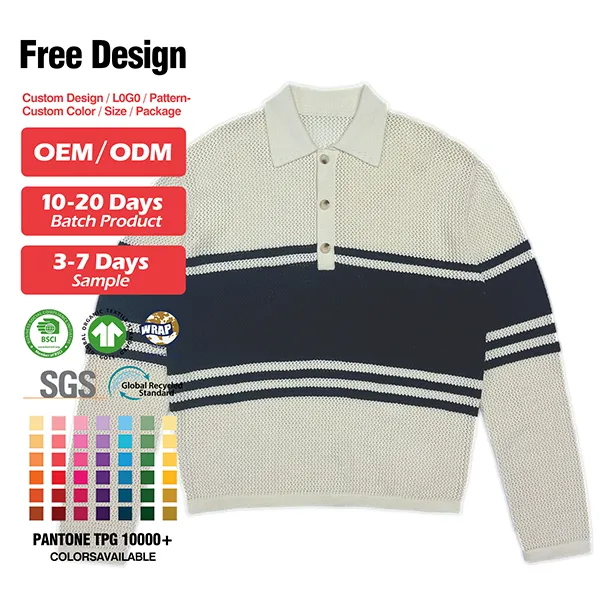
Striped Polo Knit Sweater: Classic Open-Work Textured Pullover with Button Placket, OEM Manufacturer Production
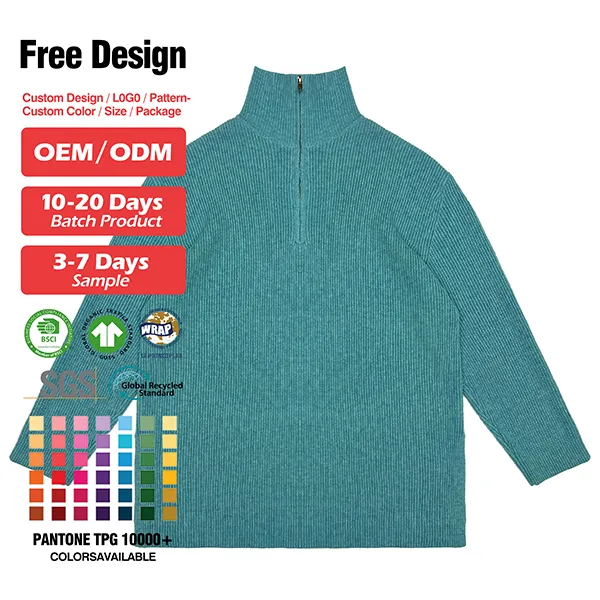
Half-Zip Ribbed Mock Neck Knit Sweater Polo Premium Textured Pullover with Metal Zipper OEM Manufacturer Production
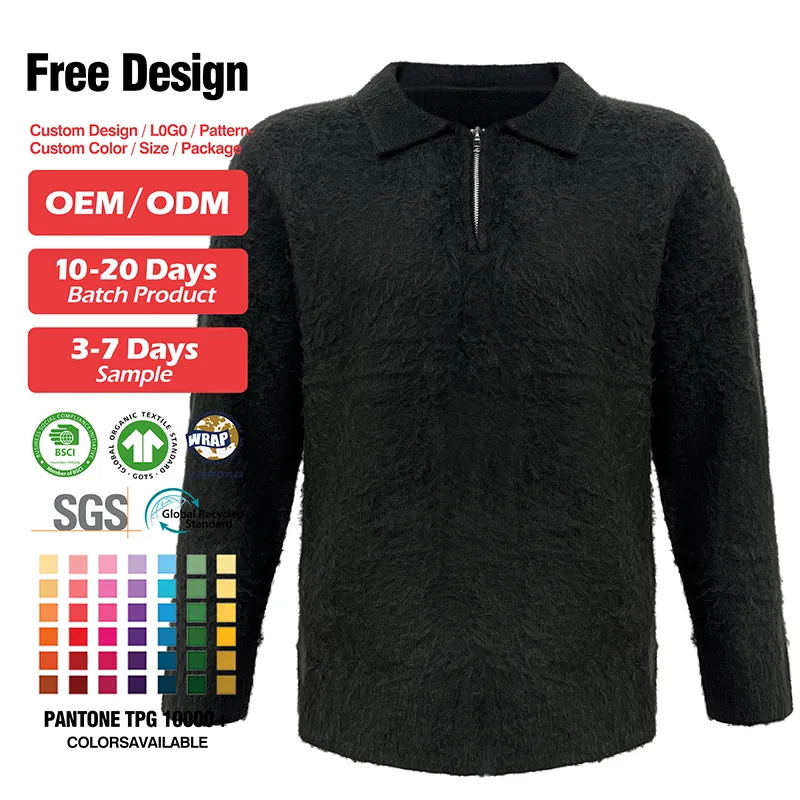
OEM Quarter-Zip Fuzzy Sweater: Private Label Brushed Mohair-Look Pullover from Manufacturer for Streetwear Brands
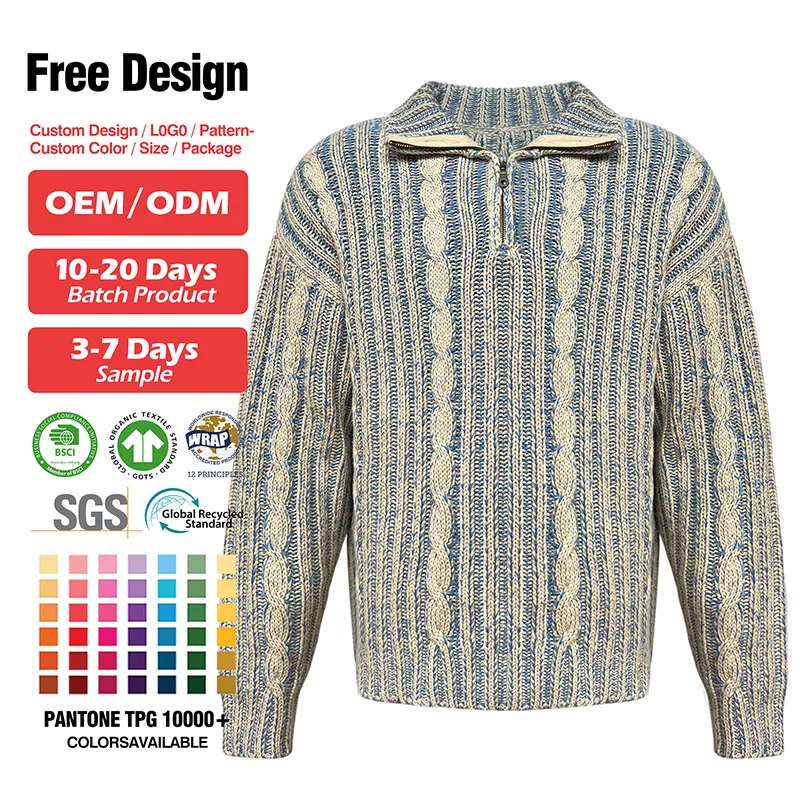
Custom OEM Quarter-Zip Cable Knit Sweater: Private Label Marled Pullover from Manufacturer for Menswear Brands
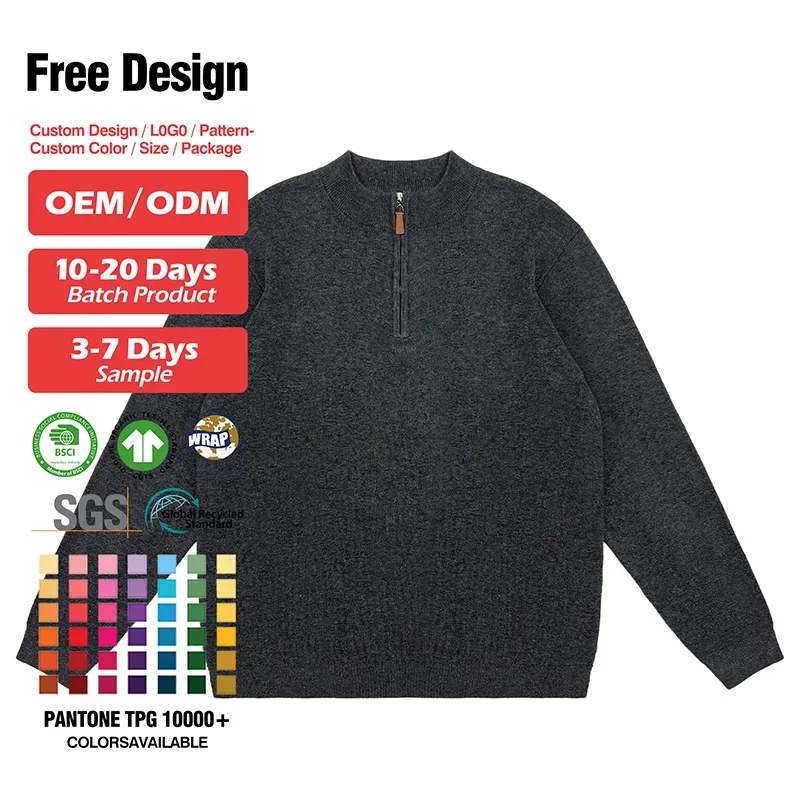
Classic Quarter-Zip Mock Neck Sweater: 12GG Fine Knit Pullover from Leading Manufacturer for Timeless Smart Casual Looks
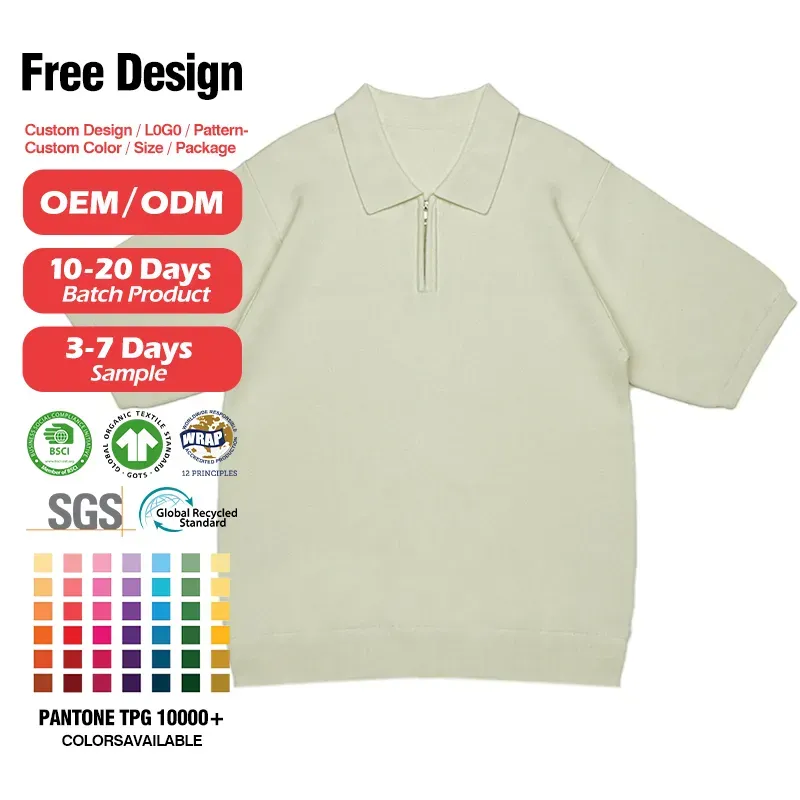
Minimalist Quarter-Zip Knit Polo: Short Sleeve 14GG Fine Gauge Sweater from OEM Manufacturer for Luxury Casual Looks
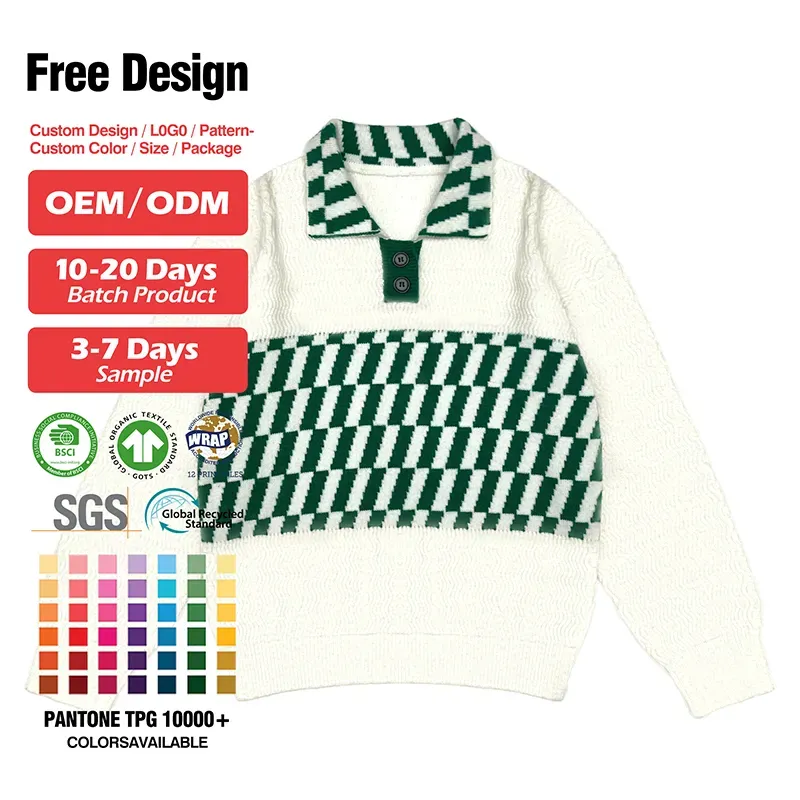
Retro Checkered Jacquard Polo Sweater from OEM Manufacturer: Cable Knit Mixed Pattern Pullover with Contrast Collar
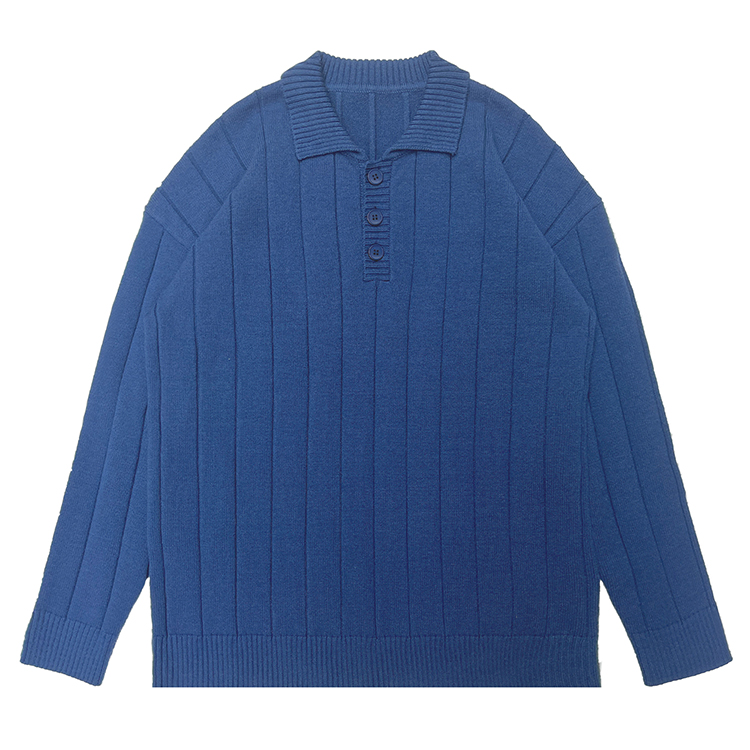
Logo Men's Youth Plain Knitwear Custom Polo Collar Long Sleeve Knitted Sweater Jacquard Letter Polo Neck OEM Supplier
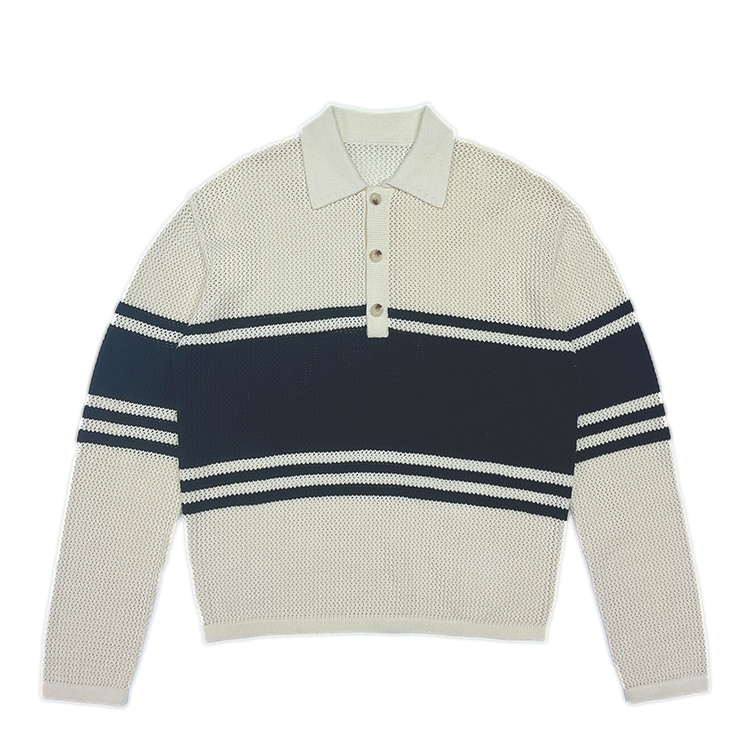
Logo Men's Striped Knit Custom Sweater Long Sleeve Winter Polo Collar Pattern Anti-Pilling Knitwear OEM Factory
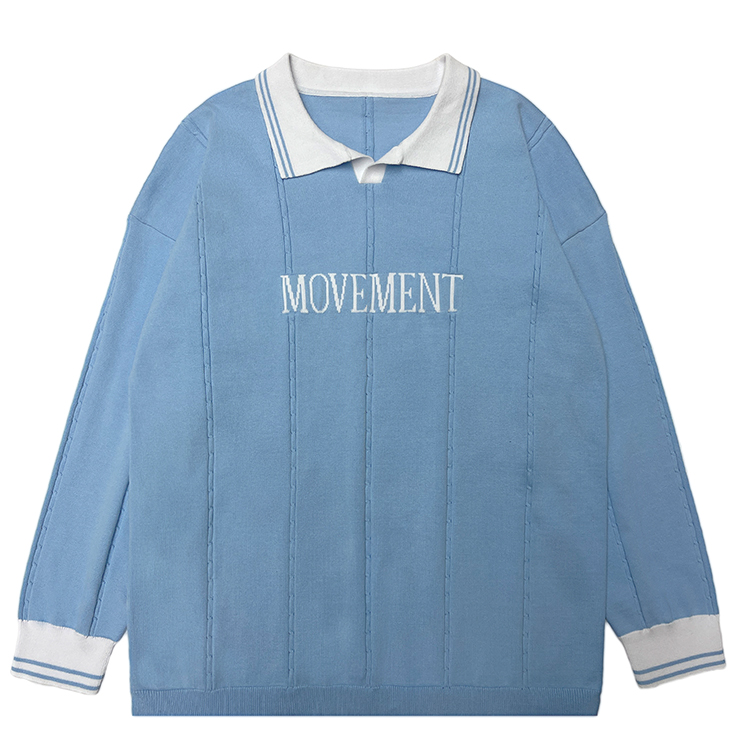
Logo Men Sweater Knitwear Long Sleeve Custom Polo Neck Knitted Sweater OEM Apparel Manufacturer
Manufacturing Process
-
Project Consultation
Tell us what you’re building. We’ll review your tech pack or ideas, clarify specs, and advise on fabrics, fit, minimums, and estimated costs—everything you need to get started with confidence. -
Sourcing Materials
Reliable sourcing tailored to your needs. We work with trusted fabric suppliers to source the best quality materials within your budget. Choosing in-stock fabrics can help reduce lead time significantly. -
Sample Making
Your first product, handcrafted. Our skilled sampling team will cut and sew your sample for fit testing, design verification, and internal evaluation before send to you for review. -
Proto Revisions
We fine-tune, you approve. Need changes? We’ll revise based on your feedback quickly—most projects only take 1–2 rounds thanks to our experience and attention to detail. -
Bulk Production & QC
Mass production with full quality control. Once approved, your design goes into production. Our QC team monitors each stage to ensure consistency, durability, and compliance with your standards. -
On-time Delivery
Reliable shipping, wherever you are. We coordinate the packaging, documentation, and logistics to ensure your order is shipped on time, whether by sea, air, or express courier.
Trending Knits
-
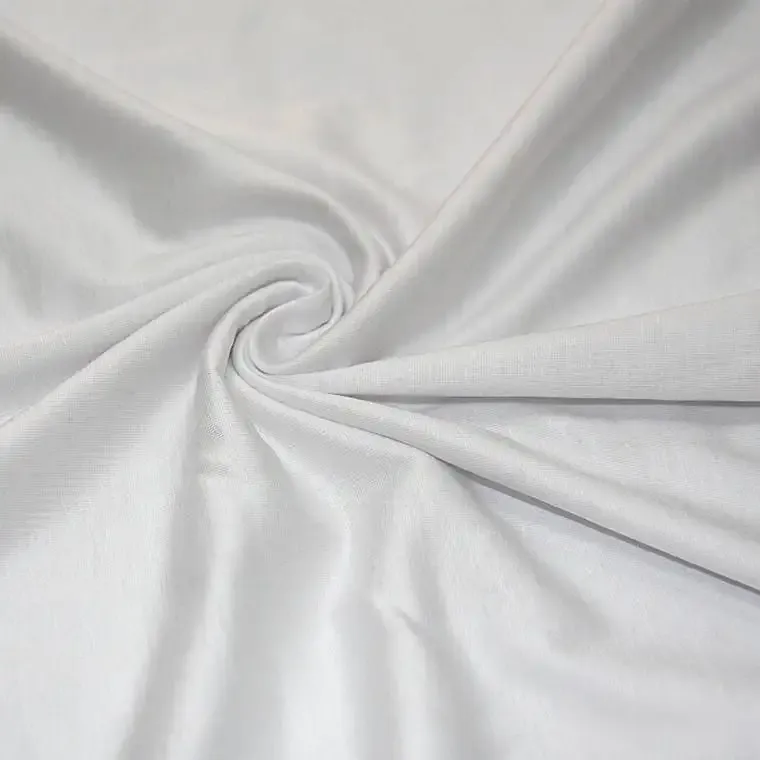
Double Mercerized Cotton
Our men's sweater factory utilizes premium cotton subjected to a dual-tension treatment. Upon expansion, its fibers exhibit a silky luster, boast a 20% increase in strength. Cool to the touch and highly breathable, it's the perfect foundation for creating luxurious, comfortable apparel.
-
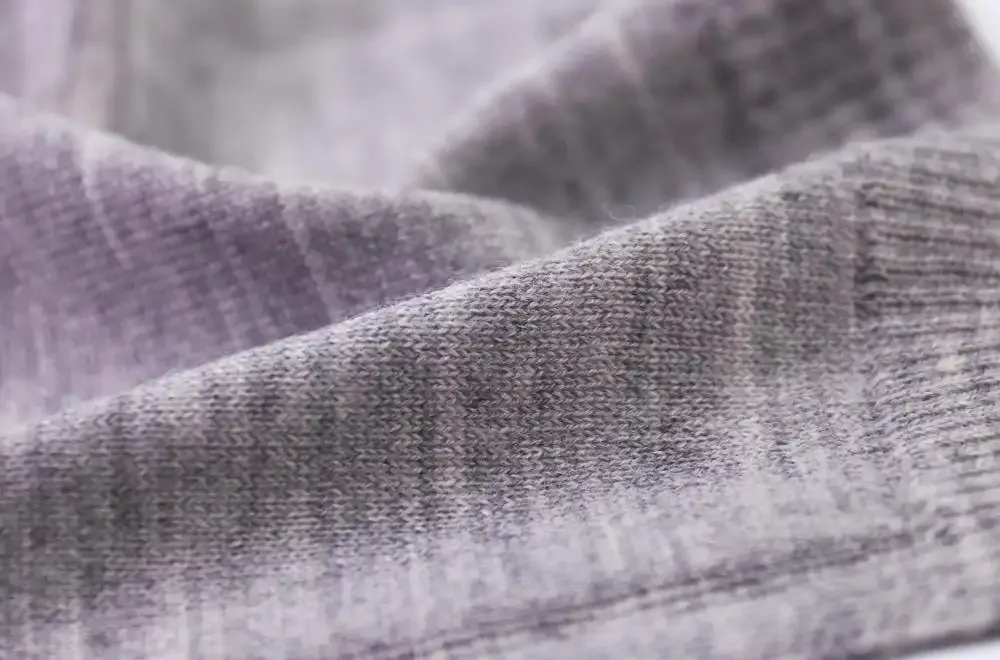
Superfine Merino Wool
We offer premium Merino wool treated with the Total Easy Care® process. As men's sweater manufacturers, we've eliminated itchiness by smoothing the fiber scales, while its natural crimp ensures elasticity and breathability—ideal for premium close-fitting knitwear.
-
Anti-pilling Acrylic Blend
As a trusted men's sweater wholesale supplier, we offer an Anti-pilling Acrylic Blend that combines durability with easy care. This fiber resists pilling, retains vibrant color, and stays smooth wash after wash — a reliable choice that meets the demands of volume production.
Men's Polo Sweater: The Ultimate Sourcing Guide for Premium Knitwear
In today's menswear landscape, the men's knit polo sweater has moved well beyond its casual roots. It fills a crucial gap between rigid formal shirting and the over-familiar t-shirt, delivering a refined fabric hand-feel and a structured silhouette that anchors the "smart casual" category.
Forward-thinking brands and premium buyers are taking note. Over recent sourcing cycles, we've seen a sustained upswing in overseas inquiries for high-quality knit polos. The end consumer is no longer content with standard synthetic blends; they're actively seeking pieces that offer skin-friendly softness, shape retention, and a premium drape. This means the competitive edge has shifted decisively from mere styling to fabric integrity and manufacturing execution.
How do you capture this category opportunity? As a specialized knitwear manufacturer with deep roots in the sector, JM Sweater understands the supply chain dynamics that drive high-margin bestsellers. This sourcing guide strips away the fluff and delivers a no-nonsense breakdown—from core yarn selections and precision knitting capabilities right through to agile OEM/ODM customization. Our goal is straightforward: to show you exactly how the right backend manufacturing partner enables you to build a men's knit polo line that genuinely stands out in a crowded market.
-
Selecting the Best Yarns: Natural and GRS-Certified Fibers
Explore premium materials like Sea Island Cotton, extra fine merino wool, and sustainable ESG-compliant blends.
-
Advanced Knitting Technology: Precision from 2G to 18GG
Learn about our high-precision manufacturing capabilities using industry-leading STOLL and Shima Seiki machines.
-
Premium Construction Details: The Value of Hand-Linking
Understand how seamless hand-linking and refined collar designs elevate garment quality and comfort.
-
OEM & ODM Customization: Flexible Solutions and Low MOQ
Discover our end-to-end manufacturing services, agile low-MOQ policies, and bespoke branding options.
-
Quality Assurance and International Compliance
Review our rigorous in-house physical testing standards and global trade compliance protocols.
-
Partner with a Reliable Knitwear Manufacturer
Connect with the JM Sweater team to request yarn swatches and start your custom production.
-
Frequently Asked Questions (FAQ)
Get quick answers regarding our MOQs, recommended knitting gauges, and sustainability practices.
Selecting the Best Yarns: Natural and GRS-Certified Fibers
Yarn selection is the make-or-break foundation for any men's knit polo sweater. The fabric's hand-feel, drape, and luster directly translate to a tangible price premium at retail—often tens or even hundreds of dollars apart.
1. Premium Natural Fibers for High-Value Haptics
For mid-to-upper-tier men's polo sweaters, Sea Island Cotton and extra fine merino wool remain the gold standard. Sea Island Cotton delivers exceptionally long, fine staples that spin into yarns with a silky sheen and unmatched breathability—an ideal match for lightweight spring and summer knits. Extra fine merino wool, on the other hand, offers natural thermoregulation and wrinkle resistance, giving garments that sought-after structured drape and elevating the brand's perceived value.
2. GRS-Certified Sustainable Yarns: Meeting European and US ESG Compliance
With ESG compliance scrutiny tightening across European and American buyers, traceable sustainable materials have moved from "nice-to-have" to "non-negotiable." JM Sweater's raw material network is deeply integrated with GRS-certified recycled cotton, recycled polyester, and eco-friendly recycled wool blends. This not only helps brands navigate rigorous cross-border supply chain audits but also aligns with the growing sustainability consciousness in Western consumer markets.
3. Technical and Functional Blends: Balancing Frequent Wear and Shape Stability
Pure natural fibers perform beautifully, but they can fall short on dimensional stability after repeated washing. Strategic blending—such as cotton/silk/nylon or wool/anti-pilling acrylic mixes—retains that natural skin-friendly touch while significantly improving elastic recovery, pilling resistance, and wash durability. The result: a men's knit polo that keeps its collar shape and side seams smooth, wash after wash.
Advanced Knitting Technology: Precision from 2G to 18GG
Knitting techniques and machine precision set the ceiling for your polo sweater's fit and quality. A clean, even fabric surface, accurate width control, and consistent pattern presentation all trace back to the hardware on the production floor.
1. Cutting-Edge Machinery for Precision Knitting
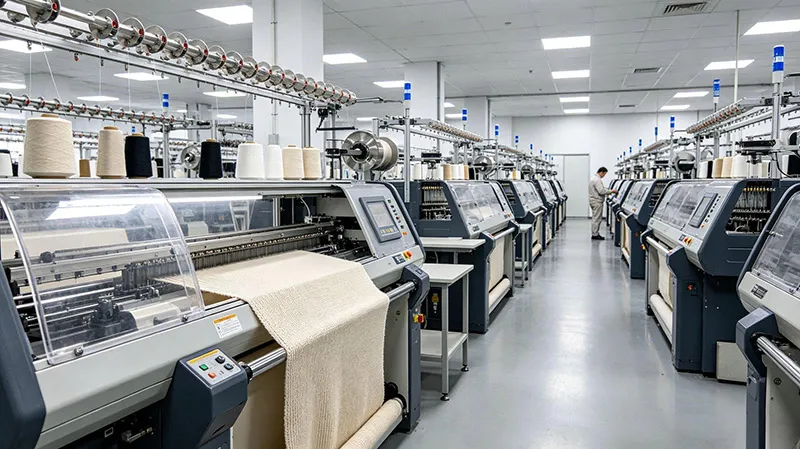
To ensure consistent quality across bulk production and meet tight delivery schedules, JM Sweater's production facility is equipped with industry-leading STOLL and Shima Seiki computerized flat knitting machines. The precision parameters these machines offer minimize tolerance drift in rib stretch recovery and garment dimensions—eliminating the "same size, different fit" issues common in smaller, less equipped workshops.
2. Full Gauge Range: From 2G to 18GG
Our factory handles the full spectrum, from chunky 2G to ultra-fine 18GG. Whether you're developing heavyweight winter polos with pronounced textural cable patterns and Aran motifs, or ultra-lightweight summer business styles that prioritize breathability, we have the production capability to match your requirements precisely.
3. 14GG – 18GG Fine Gauge: The Defining Factor for Premium Business Polos
For business and light-luxury polo shirts, fine-gauge knitting in the 14GG to 18GG range is where high-value differentiation happens. Higher stitch density yields a fabric with exceptional compactness and a smooth, almost silken hand-feel. The resulting garment drapes cleanly against the body, minimizes sheerness, and delivers a crisp, refined look—even when worn close to the skin.
Premium Construction Details: The Value of Hand-Linking
In men's knit polo sweater manufacturing, the perception of quality is often determined by the details you don't immediately notice—the seams, the collar, the finishing touches. These subtle production choices are precisely what separates commodity-grade goods from true premium offerings.
1. Hand-Linking: The Benchmark for Flat, Seamless Construction
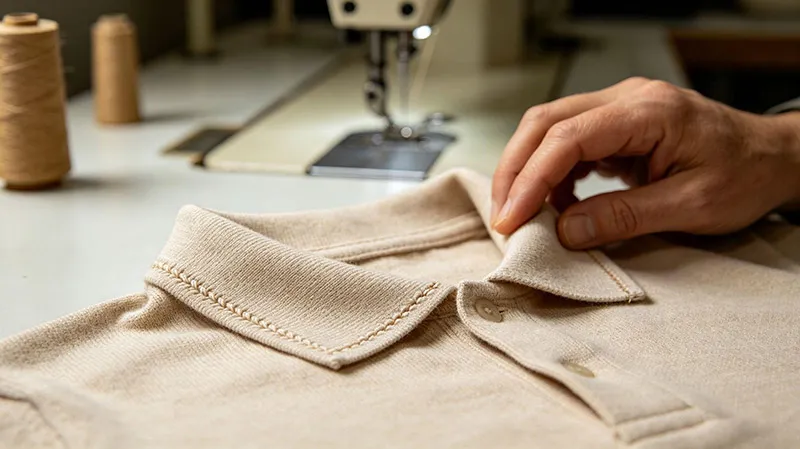
Unlike the overlock cut-and-sew shortcuts common in fast fashion, JM Sweater employs hand-linking for the collar, shoulder, and armhole connections on our premium polo lines. Experienced technicians manually match each loop on a linking machine, stitch for stitch. This method eliminates the bulky ridges found in conventional seaming, producing flat, smooth joints that sit comfortably against the skin with zero irritation. The result is a collar and shoulder line that follows the body's natural contours without sacrificing durability.
2. Collar and Placket: Defining the Garment's Character
The collar sets the visual tone for any polo. We offer a range of collar constructions to suit different brand aesthetics: a dress-shirt style standing collar with interlining prevents curling after washing for a sharp business look; the elegant Johnny collar delivers a relaxed, resort-inspired vibe. Paired with natural shell buttons or genuine corozo nut fastenings, these small details speak volumes about overall quality.
3. Ribbed Trim: Locking in Shape and Longevity
Cuffs and hem are reinforced with high-elasticity spandex yarns to prevent sagging or distortion after extended wear and repeated laundering. The controlled tension at these finishing points ensures the hem sits naturally at the waist, maintaining the clean, structured outline that defines a well-made polo sweater.
OEM & ODM Customization: Flexible Solutions and Low MOQ
In a competitive menswear market, a brand's ability to respond quickly to shifting trends while managing inventory risk depends heavily on supplier agility. JM Sweater leverages a mature supply chain infrastructure to deliver efficient, reliable, and fully customizable OEM/ODM services for men's knit polo sweaters.
1. One-Stop OEM/ODM Solutions
We manage the entire journey—from initial concept and tech pack development, through sampling and revision, right up to final bulk production. Whether you need to translate a designer's sketches into a manufacturable style (OEM) or require our insights to develop trend-forward bestsellers from scratch (ODM), our experienced technical and R&D teams are equipped to bring your vision to life with precision.
2. Flexible Low MOQ Support
To support emerging designer brands, independent boutiques, and established labels testing new seasonal capsules, JM Sweater offers competitive low MOQ policies. This approach reduces upfront capital commitment and inventory carrying costs, while enabling agile, small-batch reorders across multiple SKUs.
3. Comprehensive Detail Customization
In an era of product homogenization, distinctive details build brand recognition. We can tailor your men's knit polo sweater across multiple dimensions to align with your brand identity:
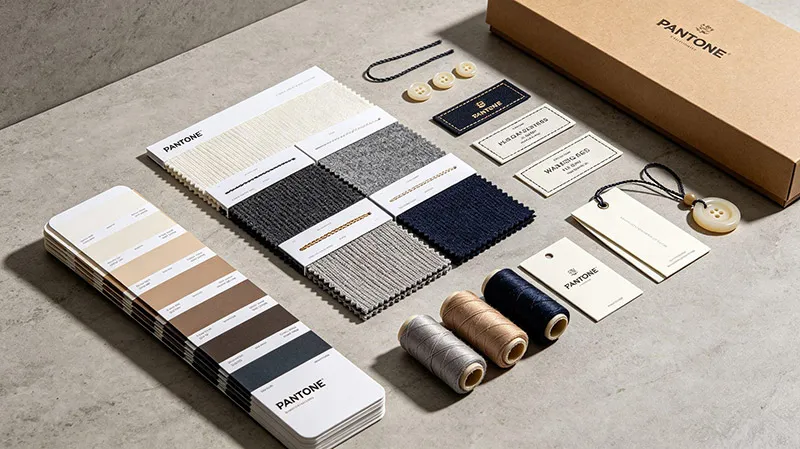
- Yarn and Color: Pantone-matched dyeing or rapid in-stock color sampling.
- Trims and Branding: Custom-woven labels, care instructions, hang tags, and bespoke metal or resin buttons.
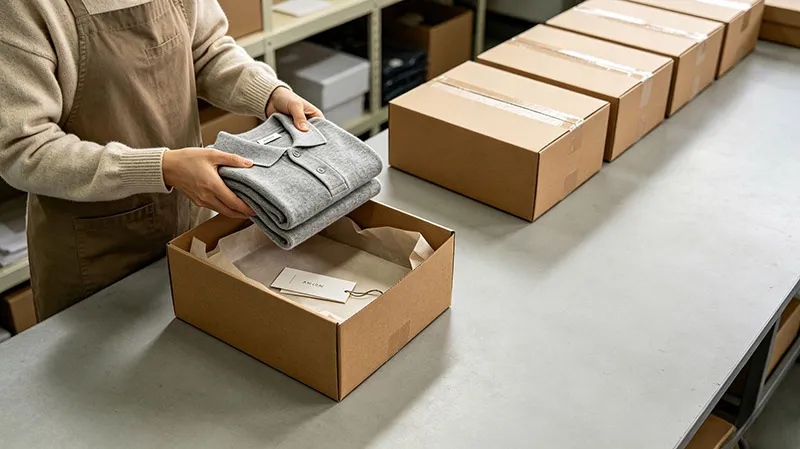
- Packaging: Eco-friendly paper bags, gift boxes, or custom-branded cartons to reinforce your brand presentation at every touchpoint.
Quality Assurance and International Compliance
For cross-border buyers, product consistency and regulatory compliance are the bedrock of a successful partnership. JM Sweater operates under a rigorous quality management and compliance framework to ensure every shipment of men's knit polo sweaters withstands the scrutiny of demanding international markets.
1. Stringent In-House QC Standards
Our quality control team conducts comprehensive physical performance tests both during and before bulk shipment. Core testing parameters include:
- Dimensional Stability: Precise control over shrinkage and torque after washing, ensuring the garment retains its original fit over time.
- Colorfastness: Rigorous testing for wash, perspiration, and rubbing fastness to eliminate dye bleeding or transfer issues.
- Pilling Resistance: Professional pilling assessments on merino wool and cotton blends to maintain a clean, fresh appearance through the garment's lifecycle.
2. Global Trade and Safety Compliance
For our key export markets in Europe and North America, all products comply with relevant international safety regulations and trade standards. Whether it's flammability requirements for specific fabric types or restrictions on hazardous chemical residues, we provide compliant test reports and certification support—removing the guesswork from customs clearance and regulatory audits.
Partner with a Reliable Knitwear Manufacturer
Securing a dependable knitwear manufacturing partner is the critical success factor for any men's knit polo sweater brand. From sourcing premium Sea Island Cotton and extra fine merino wool, through fine-gauge 18GG knitting and meticulous hand-linking, to flexible low-MOQ OEM/ODM support—JM Sweater is committed to delivering exceptional quality and stable supply chain performance for global buyers.
We understand that great garments require more than technical skill; they demand efficient communication and on-time delivery. Whether you're building a high-margin luxury diffusion line or testing a new seasonal concept, a capable manufacturing partner gives your brand the competitive edge it needs to thrive.
Ready to elevate your menswear collection? Reach out to the JM Sweater technical and sales team today. Request complimentary yarn swatches, discuss your design concepts in detail, or obtain a tailored, obligation-free quote. Let's translate superior knitting craftsmanship into tangible commercial value—together.
Frequently Asked Questions (FAQ)
We can customize sweaters of various categories.
Sweater Factory Video
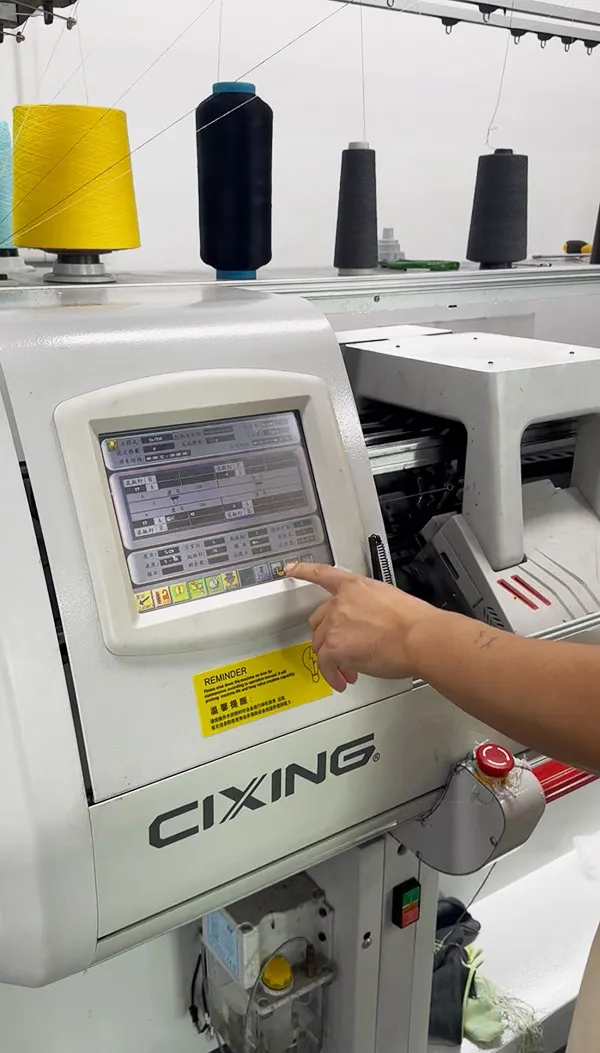
Sweater Manufacturer Sample Room: OEM/ODM Sampling, Pattern Making & Knitting Programming
Duration: 29sUpdated: September 23rd, 2026A detailed walkthrough of our knitwear sample room, showcasing how a professional Private Label Sweaters Manufacturer manages the complete development cycle from client tech pack interpretation to finished prototype approval. The video highlights skilled technicians creating computerized flat knitting programs on German STOLL and Japanese Shima Seiki software, alongside patternmakers calculating stitch density, yarn tension, and shrinkage allowances. Key sampling operations featured include automated panel knitting across 3G, 5G, 7G, 12G, and 14G gauges, precision hand-linking for seamless collar and shoulder joining, manual thread trimming, and steam framing for dimensional stability. Designed to support B2B buyers and fashion designers, this sample development center handles custom proto samples, fit samples, color lab dips, and pre-production samples (PPS) utilizing organic cotton, merino wool, fine cashmere blends, and recycled yarns.
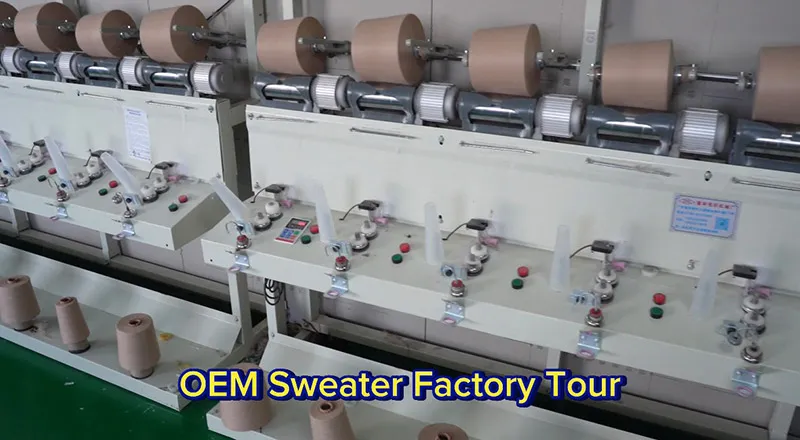
Inside a Leading Knitwear Manufacturer in China – Factory Tour & Behind the Scenes
Duration: 58sUpdated: August 10th, 2026Welcome to our knitwear manufacturing facility in Guangzhou, China. This video takes you behind the scenes of our 3,000-square-meter factory, where we produce high-quality knitted garments for brands worldwide. As a leading sweater manufacturer in China, we specialize in custom OEM and ODM production across five core categories: men's knitwear, women's knitwear, children's knitwear, pet knitwear, and a full range of knitwear accessories. Men's Knitwear & Women's Knitwear Our factory is equipped with over 110 advanced STOLL computerized flat-knitting machines, capable of producing everything from classic crewneck sweaters and V-neck pullovers to fashion-forward cardigans and knit tops for men and women. With a gauge range of 1.5GG to 18GG, we can handle chunky cable knits as well as fine-gauge lightweight styles. Whether you need a bulk order for a retail chain or a small batch for a startup brand, our flexible production lines ensure consistent quality and on-time delivery. We work closely with fashion brands, wholesalers, and importers across North America, Europe, and Australia, offering full-service support from yarn selection to finished garment inspection. Children's Knitwear & Pet Knitwear Our expertise extends to children's knitwear and pet knitwear – two fast-growing segments in the global apparel market. For kids, we produce soft, durable, and safe sweaters in a wide range of colors and styles, from school uniforms to casual wear. All children's garments are crafted from certified materials that meet international safety standards. For pets, we are a trusted manufacturer of custom dog and cat sweaters, offering breed-specific sizing, premium yarns, and creative designs that keep pets warm and stylish. Whether you are launching a pet apparel line or expanding your children's collection, our low MOQ and fast sampling service make it easy to get started. Knitwear Accessories Beyond sweaters, we are also a leading manufacturer of knitwear accessories – including beanies, scarves, gloves, headbands, and knit hats. These accessories are produced using the same high-quality yarns and precision knitting techniques as our garments, ensuring a cohesive look and feel across your entire product line. With our in-house design team, we can develop custom patterns, colors, and branding elements to match your collection's aesthetic. Behind the Scenes: Our Process In this video, you will see every stage of our production process – from yarn intake and quality inspection to computerized knitting, linking, washing, and final quality control. Our facility is certified under GRS, BSCI, WRAP, ISO 9001, and OEKO-TEX, reflecting our commitment to ethical manufacturing and environmental responsibility. We also maintain a dedicated sample showroom where clients can review fabric swatches, gauge samples, and finished prototypes before placing bulk orders. Why Choose Us? As a direct knitwear manufacturer in China, we offer factory-direct pricing, transparent communication, and a dedicated account management team for every project. Whether you need men's knitwear, women's knitwear, children's knitwear, pet knitwear, or knitwear accessories, we are your one-stop partner for reliable, high-quality production. Book Your Factory Tour Today We welcome international buyers to visit our factory and see our operations firsthand. Schedule a visit to meet our team, review our capabilities, and discuss your next collection. Contact us now to arrange your factory tour!
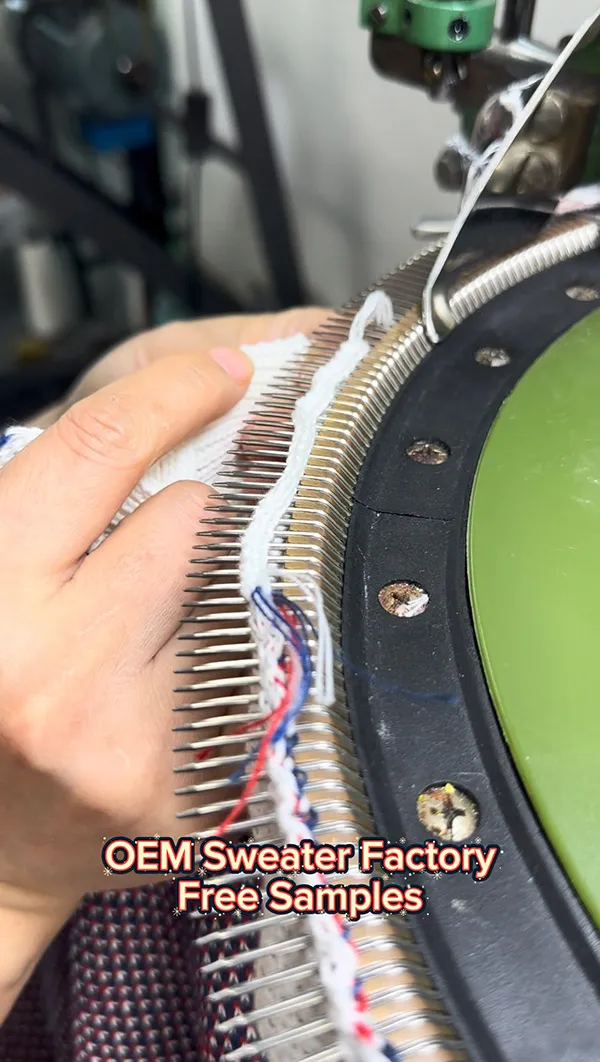
Custom Pullover Sweater: White Striped Ribbed Collar Linking Video Highlights Flat Seams and Free Sample Options
Duration: 21sUpdated: October 7th, 2026This custom pullover sweater video demonstrates how flat, clean seams are assembled for classic crewneck jumpers featuring red, white, and blue striped rib collar trims. Crafted from soft cotton or fine wool blend yarns, the elastic ribbed collar provides comfortable stretch recovery, shape retention, and a neat neckline fit. The timeless contrast tipping style adds a sporty preppy aesthetic, making it an ideal choice for casual daily wear, university streetwear, and collegiate fashion collections. Designed for independent clothing brands, our direct factory setup delivers full OEM/ODM manufacturing for every custom pullover sweater line. We offer flexible low MOQ orders, custom yarn color dye matching, private woven label integration, and free physical samples so design teams can evaluate fabric softness, weight, and seam strength before placing bulk wholesale orders.
Sweater Manufacturer Blog
Knitwear Quality Control: Complete Sweater Inspection Guide
Subtitle:Sweater Manufacturer AQL 2.5, Torquing Prevention, Gauge‑Specific Checks, and Tolerances That Hold Up on the Measuring Table In cross-border knitwear sourcing and custom production, your Quality Control (QC) setup isn't just an inspection checkpoint—it’s the single biggest factor dictating your brand’s margin and survival. Unlike standard wovens, fully-fashioned knits are built loop by loop. Variable yarn tension, moisture regain, unpredictable relaxation shrinkage, and complex panel linking make knitwear inherently dynamic on the factory floor. Over the years, as a professional sweater manufacturer I’ve seen too many brands watch their profits burn over preventable finishing errors: distorted necklines, twisted side seams, premature pilling, or a dropped loop that unravels an entire panel in transit. Left unchecked at the mill, these micro-defects land squarely on the retail side—driving up return rates, damaging retailer relationships, and triggering costly chargebacks. To protect your shipments, we’ve broken down our factory-floor inspection framework into a practical playbook for international sourcing directors, technical designers, and buyers. Below is a breakdown of the core operational protocols covered in this guide: Why standard woven inspections fail on knitwear: How yarn mechanics, gauge tension, and structural elasticity force a completely different inspection approach. The five defects that actually cost you money – and how we stop them: Root causes and real-world countermeasures for spiralling, pilling, shading, and open seams before bulk packing. AQL 2.5/4.0 – thresholds that actually get used: A breakdown of sampling sizes, defect classification (Critical, Major, Minor), and pass/fail rules on the measuring table. Gauge-specific checks: 3GG is not 12GG: Tailoring inspection parameters to match the structural risks of coarse-gauge chunkies versus fine-gauge knits. Measurement POMs and the tolerance trap: Practical flat-lay protocols and realistic tolerance sheets that eliminate stretch disputes between buyers and factory QC teams. Tech Pack must-haves + handling third-party inspectors (SGS/ITS/BV): Aligning your spec sheets and factory SOPs to guarantee clean third-party field reports and zero-defect deliveries. Whether you're an established private-label brand scaling up seasonal bulk orders or a sourcing engineer tightening up your supplier quality agreement, this guide outlines the exact protocols needed to de-risk your knitwear supply chain from cone to carton. Why standard woven inspections fail on knitwear If your QC team uses a woven‑garment checklist on sweaters, you’re effectively writing off a percentage of your order before it leaves the factory. Wovens are cut from stable cloth; knits are loops that move. Tension, moisture regain, and yarn twist behave differently on every batch. I’ve personally watched S‑twist yarns wreck a 12GG production run in our Guangzhou facility simply because the steaming cycle wasn’t adjusted for that specific lot. The side seams spiralled so badly we had to pull the whole batch at the lightboard. The structural shift is simple: a broken thread in a woven stays local; a dropped loop in a knit can ladder the entire panel. So we measure different things: Tension & stress release – if the knitting stress isn’t steamed out, the garment shrinks or twists in the first home wash. Moisture regain – batch‑to‑batch humidity changes shift finished dimensions more than most buyers realise. Torquing – unbalanced single‑ply twist creates that ugly spiral effect. You can’t iron it out, and you can’t press it flat. We run three dynamic tests on every style: neck/cuff recovery (stretch it and see if it snaps back), light‑board scanning (every piece, no exceptions), and shade matching under D65/TL84 before linking. That last one catches dye‑lot mismatches that would otherwise only show up after packing. The five defects that actually cost you money – and how we stop them Defect What causes it Our fix on the floor Torquing / seam twist Over‑twisted yarn or uneven steam setting Pre‑knit reaming to relax twist; we slow the feed tension on the machine if the yarn feels tight; high‑temp steam set after knitting Pilling Short‑staple fibres or too much softener in the wash Switch to long‑staple/combed yarn; run a Martindale test at sample stage – if it scores below 3.5, we don’t cut Dropped stitches / holes Worn latch needles or poor linking Daily needle changes; 100% light‑board scan – zero tolerance. One hole, out of the shipment. Shading / dye‑lot variation Different dye batches or unstable vat temp Strict dye‑lot control; we hold back trims and body panels until they’re matched side‑by‑side under the lightbox Wash‑induced shrink No pre‑shrink allowance or mismatched blend rates Build 3‑5% shrink into the knitting programme; wash‑test the pilot sample and adjust before bulk Here’s a dirty little secret that doesn’t make it into the textbooks: some factories over‑stretch the rib during finishing just to hit the chest measurement on the table. That rib snaps back in transit, and suddenly your spec sheet is worthless. We check the relaxed state specifically to catch that – not the stretched number the production line wants to show you. AQL 2.5/4.0 – thresholds that actually get used We run General Inspection Level II for final random inspection. Critical defects are AQL 0 – one broken needle or a missing fibre label and the whole order stops. For a 2,000‑piece order, we pull 125 pieces. If we find 7 Majors and 10 Minors, the batch rolls. If Majors hit 8, we reject it on the spot. No debate. Real‑world classification (knits only): Major – dropped stitch, open linking seam, side‑seam twist >3%, measurement out of spec, obvious shading. Minor – loose thread >1cm inside, misplaced hang‑tag, light press mark. I’ve had third‑party inspectors flag a 2cm length difference on a heavy 5GG cable knit. We stopped the inspection, let that sweater relax flat for the full 24 hours, and re‑measured. It came back within tolerance. They signed the field report. That’s why we always build a relaxation hold into the FRI schedule – and we insist the inspector watches the re‑measure. Gauge‑specific checks: 3GG is not 12GG Coarse (3‑5GG) – gravity is your enemy. We never hang these; we measure after 24 hours flat. Linking strength gets a hard pull test at the shoulder. Mid (7‑9GG) – torquing and rib recovery are the trouble spots. We check side‑seam twist (must be ≤3%) and stretch neck/cuffs to verify snap‑back. If the rib doesn’t return, we add spandex in the next run. Fine (12‑14GG) – micro‑holes and density. 100% lightboard scan; we use a density glass to check courses and wales per inch and hold ±3% across the batch. Measurement POMs and the tolerance trap Never measure straight out of the polybag. That’s a rookie mistake that costs buyers thousands in false chargebacks. Our protocol: flat‑lay for 2‑4 hours (24 hours for coarse gauges), no stretching, non‑stretch steel tape. Core POMs we actually use: Body length – HPS to hem (including rib) Chest width – half measure, 1” below armhole Shoulder – seam to seam Sleeve length – from CB neck to cuff Neck width/depth – at seam and from back neck to front dip Tolerance sheet (by gauge): POM Fine (12‑14GG) Mid (7‑9GG) Coarse (3‑5GG) Heavy texture Body length ±1.0 cm ±1.2 cm ±1.5 cm ±2.0 cm Chest (half) ±0.8 cm ±1.0 cm ±1.5 cm ±1.5 cm Shoulder ±0.8 cm ±1.0 cm ±1.2 cm ±1.5 cm Sleeve ±1.0 cm ±1.2 cm ±1.5 cm ±2.0 cm Neck ±0.5 cm ±0.8 cm ±1.0 cm ±1.0 cm If the yarn has high spandex content, we add 0.3‑0.5cm on horizontal measures – but we flag that in the Tech Pack before production, never after the fact. Tech Pack must‑haves + handling third‑party inspectors (SGS/ITS/BV) Over 40% of disputes we mediate come down to one thing: the Tech Pack doesn’t specify the relaxed state. Yours must include: Yarn blend and count (e.g. 2/28NM) plus dye method Gauge and stitch structure, with a max float‑length limit A clear POM diagram – not just text Pantone reference and light‑source priority (D65 > TL84) Label position, thread spec, and packing details Performance numbers: pilling ≥3.5, colourfastness ≥4, shrink ≤3% For the 3rd‑party inspector: we give them a dedicated table, lightbox, and lightboard. The checklist they use must match the approved PP sample to the letter – no last‑minute tolerance changes. If they flag an out‑of‑spec measurement, our QC lead has the right to stop the process, re‑relax the piece, and re‑measure on the spot. We photograph the disputed point, sign the field report together, and keep a sealed sample for appeal. Final word (straight to the point) Knitwear quality isn’t inspected in at the end – it’s built into the yarn tension, the relaxation time, and the gauge‑specific checkpoints. If your Tech Pack doesn’t already specify the relaxed state and the recovery test, we’ve got a gap to close before we cut a single cone of yarn. If you’re sourcing knitwear and want a partner who runs these protocols daily – and who will flag the risks before they become chargebacks – send your Tech Pack over. Our technical team will give you a no‑cost feasibility read, a tolerance sample to check our finishing standards, and a supply‑chain risk review specific to your next season.
view more
How to Choose a Knitwear Manufacturer: Complete Buyer Checklist
How to Choose a Knitwear Manufacturer: Complete Buyer Checklist A Step-by-Step Sourcing Guide for Brands — Even Without a Tech Pack Sweater Manufacturer demand is rising as the global knitwear market is projected to surpass $1 trillion by 2035, with demand for high-quality sweaters continuing to grow. But for brand founders, capturing this growth isn't easy. Let’s cut the flattery. Finding a sweater factory isn’t about winning a lowball bidding war. In my experience, the cheapest quote usually comes with hidden costs: missed ship dates, inconsistent sizing, pilling after two washes, and a communication blackhole that makes you want to pull your own hair out. Smart sourcing isn’t about price. It’s about finding a manufacturing partner that’s responsive, transparent, and technically competent. Even if you don’t have a technical designer on staff or a fully built-out tech pack, you can screen factories quickly using these four core criteria. Here’s exactly how. 1. Hardware & Process: What’s Actually on the Floor Forget the glossy sales pitch. A factory’s real capability comes down to two things: the knitting machines they run and how they stitch the pieces together. Gauge (GG) Selection & Machine Capability Gauge refers to the number of needles per inch on the knitting bed. Higher GG = finer, lighter fabric. But here’s the catch: a factory needs the native machine for each gauge. You’re looking for STOLL (Germany) or SHIMA SEIKI (Japan) equipment, not knockoffs. Here’s how the gauges break down: Coarse Knit (3GG – 5GG): Heavyweight fall/winter sweaters, cable knits, cardigans. This gauge tests a factory’s tension control on wide-gauge beds. Mid-Gauge (7GG – 9GG): Your bread-and-butter spring/fall styles. This is the volume sweet spot. The key metric here is stitch uniformity across bulk production. Fine & Superfine (12GG – 18GG): Base layers, fine merino, and cashmere blends. This is where the factory’s climate control and finishing processes get scrutinized. Temperature and humidity swings wreck fine-gauge production. Red flag: A factory that claims they can run 7GG on a 12GG machine by "modifying" the settings. That’s a fancy way of saying your sweater will stretch out and lose its shape after one wear. Walk away. The Joining Process: What Determines Garment Durability This is the single biggest differentiator between a premium sweater and fast-fashion garbage. Hand-Linking (Looping): Each stitch from the knitted panels is looped onto a linking machine, one by one. The result? Seams that are flat, elastic, and almost invisible against the skin. This is how you build garments that last. Cut-and-Sew (Overlock): The cheaper, faster route. Panels get cut with scissors and stitched together with an overlock machine. The seams are bulky, have zero give, and will start fraying at the edges after a few wash cycles. Bottom line: if you’re selling a premium product, hand-linking is non-negotiable. If you’re chasing ultra-low cost, just know the trade-offs. 2. Decoding MOQ: How to Test the Waters Without Breaking the Bank Here’s a truth most brand founders learn the hard way: the MOQ bottleneck usually isn’t the factory’s knitting machines. It’s the dye house. Most mills set dye-lot minimums at 100–300 kg per color. That translates to roughly 300–1,000 finished garments, depending on weight. So how do you get started with 100–200 pieces? Stock service yarns. Stock Service vs. Custom Dyeing If you insist on a specific Pantone match, be prepared to pay for custom dyeing—and wait an extra 2–3 weeks for lab dips and strike-offs. But if you’re willing to work from the factory’s stock yarn color cards, everything changes. Criteria Stock Service Yarns Custom Dyeing MOQ Low (100–200 pcs/design) High (300–1,000+ pcs/design) Lead Time Fast (3–7 days for strike-offs) Slow (adds 2–3 weeks for color development) Risk Low—test multiple colors easily High—you’re sitting on leftover yarn Pro tip: When you send your RFQ, ask this exact question: “What’s your MOQ if we use your stock service yarns?” The answer will tell you immediately if they’re set up for agile, small-batch production or if they’re still operating in the old-school volume model. 3. Sampling Without a Tech Pack & Rigorous Quality Control A good OEM/ODM factory is essentially a development partner. They don’t need a perfect tech pack to start working with you. How to Kick Off Sampling Send them any one of these: High-res reference images or sketches—clearly mark the silhouette and pattern details you want. A physical sample garment—this is the gold standard. Even if it’s the wrong fabric or a different brand, they can reverse-engineer the measurements and build a new pattern from it. The Three Critical Samples Before Production Don’t skip these. Each one protects you from expensive mistakes. Knit-down (Yarn Swatch): This is your first sanity check. It confirms the actual yarn hand-feel, the true color, and how the stitch pattern renders. Approve this before the factory cuts a single panel. Proto Sample (First Fit Sample): This is your first look at actual garment silhouette and construction. Check the fit, the drop, the armhole depth. This is where you catch pattern issues. PPS (Pre-Production Sample): This is the non-negotiable gatekeeper. The PPS must be made with 100% production yarn, trims, and finishing processes. That means the same dye lot, the same wash, the same steam-setting. Do not—under any circumstances—authorize bulk production without a signed-off PPS in hand. The Quality Benchmarks That Matter (AQL 2.5) Hold your factory to these three metrics during the final inspection: Size tolerance: Within ±1.5 cm of the spec sheet. Pilling resistance: ISO/AATCC rating of 3–4 or higher. Anything below that and your customers will complain within weeks. Washing shrinkage: Must fall within ±3% to ±5% after the standard wash-and-set finishing process. 4. Sending a Smart RFQ & Spotting Supplier Red Flags You don’t need a novel. You need a concise, information-rich inquiry that gets you a real quote on the first pass. The Four Components of a High-Conversion RFQ Include these four elements, and you’ll get a useful response—not a generic brochure. Estimated quantity: Total pieces AND breakdown per color. (Example: 200 total, 100 pcs in Navy, 100 pcs in Charcoal) Visual reference: Either a high-quality photo or simply state: “Sample garment available for shipping.” Yarn & gauge preferences: Be specific. (Example: “7GG mid-gauge, cotton-blend, using your stock service yarns.”) Target market & delivery deadline: (Example: “US market—must hit warehouse by October 15th.”) Factory Red Flags: Three to Walk Away From I’ve seen these patterns repeat across dozens of factory audits. If you hit any of these, keep looking. Slow sampling response: If they can’t turn a proto sample around on time, they’re telling you—loudly—that they can’t manage production schedules. Bulk will be worse. Pushing custom dyeing exclusively: If they refuse to show you a stock yarn color card and insist on high-MOQ custom dyeing, they don’t have a service model for emerging brands. They’re still hunting whales. No industrial steam-setting equipment: If they’re finishing sweaters with a hand iron instead of a proper steam tunnel or press, your garments will shrink and deform after the customer’s first wash. That’s a chargeback waiting to happen. Final Take: Build a Supply Chain, Not a One-Off Deal Choosing a knitwear factory isn't a transaction. It’s the foundation of your brand’s supply chain. The playbook is simple: Use stock service yarns to de-risk your initial order. Lock down your PPS before bulk production starts. Send a tight, data-driven RFQ to filter out time-wasters. Do that, and you’ll operate like a seasoned sourcing pro—regardless of your team’s size. Ready to Skip the Sourcing Headaches? Finding a knitwear partner who balances flexible MOQs, rigid quality control, and transparent communication shouldn’t feel like a gamble. At JM Sweater (Guangzhou Junma Apparel Co., Ltd.), we’ve spent 21 years perfecting custom knitwear manufacturing for growing global brands. With a 3,000 m² facility and annual capacity of 1.2M garments, we bridge the gap between high-end craftsmanship and flexible production—whether you need low-MOQ stock yarn development or full-scale OEM/ODM runs. Need help reviewing a Tech Pack or calculating yarn yield? [Get a Free Production Assessment & Quote within 24 Hours]
view more
Sweater vs. Sweatshirt: The Ultimate Guide to Differences, Manufacturing & Sourcing
What's the difference between a sweater and a sweatshirt, and which one offers higher value for your apparel brand? A complete B2B manufacturer's comparison. Table of contents Introduction & The Quick Answer The Core Difference: Manufacturing Mechanics Material Science & Sustainability Impact Brand Positioning: Aesthetics & Profit Margins B2B Sourcing Guide: MOQ and Supply Chain Conclusion: Which Should Your Brand Choose? 1. Introduction & The Quick Answer For many apparel brand founders and sourcing buyers, a sweater and a sweatshirt might look like nothing more than two different styles of pullover. But on the actual supply chain and factory floor, they represent two completely separate industrial branches. The core of the difference between sweater and sweatshirt isn't about how similar they look when worn—it's about how they're manufactured. As a B2B manufacturer deeply rooted in knitwear, we frequently need to clarify a fundamental logic for clients: sweaters belong to pure knitwear manufacturing, following the art of "yarn-to-garment" direct knitting; sweatshirts belong to the typical cut and sew industrial system. To help you see through these two categories in under a minute, we've distilled the core manufacturing parameters that determine their fate: Manufacturing Matrix Sweater Sweatshirt Forming Method Yarn directly knitted into shape (Fully Fashioned) Cut from finished fabric and sewn (Cut and Sew) Primary Equipment Flat-bed Knitting Machine Circular Knitting Machine + Cutting Floor Fabric Form Individual knitted panels Rolls of bulk fabric Core Seaming Process Linking / Looping stitch-by-stitch Overlock / Flatlock Once you understand the differences in the table above, you've grasped the lifeblood of these two categories. Whether it's factory selection, MOQ thresholds, fabric waste rates, or ultimate retail brand premium—all of it stems from this underlying manufacturing logic. Below, we'll break down the mechanical principles and optimal sourcing strategies for both garment types. 2. The Core Difference: Manufacturing Mechanics To truly understand the difference, you have to step onto the production floor. In garment engineering terms, sweaters and sweatshirts represent two fundamentally different product construction philosophies: the former is "knitting the shape," the latter is "cutting the shape." Sweater: The Art of Flat-Bed Knitting In professional sweater manufacturing, the core logic is "Yarn-to-Garment." This means there's no ready-made fabric at the start of the production line—only cones of yarn. Every inch of a sweater's texture and silhouette is "calculated" and directly knitted from scratch through machine programming. Fully Fashioned Knitting: High-quality sweater production relies on precision computerized flat-bed knitting machines (industry benchmarks like STOLL or Shima Seiki). Programming engineers write complex knit programs that control the tension and path of every yarn on the machine, directly knitting front panels, back panels, and sleeves that conform to body structure. With an industry gauge spectrum ranging from 3G (chunky) to 18G (ultra-fine), factories can precisely control a sweater's physical weight—whether it's a heavyweight chunky rib cardigan or a lightweight fine-gauge layering piece, each is shaped stitch by stitch with minimal secondary trimming required. Linking and Looping: Why do premium sweaters have virtually no stiff friction at the seams when worn against the skin? This is thanks to the sweater-exclusive linking process. Sweater seaming doesn't rely on conventional sewing machines—instead, skilled operators align the loops at panel edges stitch by stitch onto the dial needles of a linking machine. This pure yarn interlocking connection method creates extremely flat, conforming seams and gives them excellent stretch recovery. This is precisely the key technical barrier that determines a sweater's hand feel and comfort. Sweatshirt: The Efficiency of Cut & Sew By contrast, sweatshirts follow a highly standardized modern industrial mass-production route, adhering to the "Fabric-to-Garment" logic. Fabric Rolls & Cutting: The starting point of a sweatshirt production floor isn't yarn—it's finished fabric that's been custom-knitted and dyed. Upstream suppliers first use circular knitting machines to high-speed knit large rolls of fabric (most commonly moisture-wicking French Terry or insulating brushed fleece). These massive rolls are then sent to the cutting bed, where dozens of layers are stacked and flattened, then "cut" into individual component pieces according to pattern blueprints. Overlock & Flatlock: At the final assembly stage, sweatshirts use conventional overlock machines or flatlock (four-needle, six-thread) equipment. This process relies on sturdy industrial sewing thread to tightly wrap and lock the edges of two cut fabric pieces. The absolute advantage of the cut and sew system lies in its high degree of automation and production efficiency—ideal for brands with high-volume throughput. But correspondingly, its physical seams will inevitably form a slightly thick "ridge," and stretchability is limited by the sewing thread itself, unable to achieve the nearly seamless dynamic stretch of sweater linking. 3. Material Science & Sustainability Impact As the global apparel industry transitions toward ESG, European and North American brand buyers evaluating a product line no longer focus solely on garment appearance—they dig deep into supply chain environmental compliance. It's precisely in material application and sustainability dimensions that sweaters and sweatshirts demonstrate distinctly different industrial values. Fiber Choices and Tactile Feel The physical functional differences between these two garments directly determine their divergence in raw material selection. Sweatshirt materials are typically oriented toward ultimate practicality. To pursue fabric surface smoothness, moisture-wicking during exercise, and basic wind/abrasion resistance, sweatshirt fabrics mostly use pure cotton or cotton-poly blends. This fabric combination withstands high-frequency rough machine washing, but the hand feel is relatively one-dimensional—warmth is mainly enhanced by increasing fabric weight (GSM) or adding inner brushing. By contrast, a sweater's warmth mechanism doesn't rely solely on material thickness—it depends on complex knit structures (such as cable twists, Jacquard patterns) creating microscopic "still air layers" between yarns for insulation. This mechanical property gives sweaters enormous material range, enabling them to carry higher-tier fiber combinations. From Merino Wool for exceptional hand feel, to GOTS organic cotton meeting stringent organic standards, to GRS certified recycled yarns with full supply chain traceability—a sweater's rich material library offers broad space for brands to build collections with premium tactile quality. The Zero-Waste Advantage of Sweaters In apparel supply chain carbon footprint and environmental assessments, physical waste at the production end is an unavoidable hard metric. As mentioned earlier, sweatshirts depend on cut and sew processes. When cutting equipment slices fabric rolls into fixed patterns, the gaps between curved panel edges and straight-line layout are inevitable. This means that no matter how precise the nesting software, sweatshirt production unavoidably generates 10% to 15% cutting waste. This is a systematic physical loss inherent to traditional cut-and-sew industry. In contrast, flat-bed knitted sweaters have a natural structural advantage in environmental compliance. Fully Fashioned knitting follows the precise logic of "knit exactly what's needed"—equipment directly knits panel contours according to program, achieving nearly 100% yarn utilization and realizing "zero-waste production" in the industrial manufacturing sense. Furthermore, compared to synthetic-blend active sweatshirts that require high-frequency machine washing, sweaters made from natural fibers and high-quality recycled yarns require far less frequent washing, fundamentally reducing microplastics pollution entering water systems. This manufacturing attribute—zero waste at production end, low pollution at use end—aligns perfectly with current stringent international environmental regulations (such as France's AGEC circular economy law and Triman mandatory eco-labeling traceability requirements), effectively helping apparel brands mitigate compliance risks in high-standard markets like Europe and enhance green premium. 4. Brand Positioning: Aesthetics & Profit Margins For brand founders or merchandising planners, category selection ultimately returns to business fundamentals: what aesthetics it conveys for the brand, and how much profit margin it generates. In this dimension, sweaters and sweatshirts play completely different commercial roles in a brand matrix. Surface vs. Structure: How They Carry Design These two garments carry brand visuals in fundamentally different ways. Sweatshirts have a flat, dense fabric surface—a perfect canvas for screen printing, puff printing, or DTG. If your brand positioning is a streetwear label heavily reliant on bold logos and rapid graphic monetization, sweatshirts are an excellent visual canvas. Conversely, sweater design language is built on "structure." When a brand needs to enter the commercially potent "quiet luxury," "old money" aesthetic, or heavy-craft vintage streetwear market, sweater process advantages become apparent. Through Intarsia, Jacquard, and three-dimensional knit textures to present patterns, the physical depth and luxurious hand feel woven from yarn itself cannot be replaced by any surface flat print. Perceived Value and Retail Margins From the retail end, because sweaters involve more complex flat-bed programming, precision linking, and higher-tier yarn materials, they naturally command higher "perceived value" in consumer minds. In conventional apparel supply chain logic, sweatshirts often serve as volume-driving base traffic items thanks to cut-and-sew efficiency. But finely crafted flat-bed knits (sweaters) are ideal as a brand's "upgrade product line." With proper supply chain support, a sweater with unique structural texture can command a pricing ceiling far exceeding conventional sweatshirts. It not only effectively raises brand average order value but creates richer, more elastic retail profit margins. 5. B2B Sourcing Guide: MOQ and Supply Chain For B2B buyers or brand directors preparing to place purchase orders, design blueprints must ultimately land as precise supply chain data. In actual export sourcing operations, sweaters and sweatshirts face completely different rules of engagement regarding order thresholds and cross-border trade compliance. MOQ Thresholds and "Stock Service Yarns" Flexibility In the sweatshirt supply chain, MOQ is often constrained by upstream dyehouses' "fabric dye lot minimums." If you need custom brand colors for a new collection, fabric mills typically require a full dye bath (approximately 300 kg) minimum. This directly results in higher procurement thresholds for special-color sweatshirts, easily creating inventory capital pressure for startup brands or test styles. Quality sweater manufacturers, however, have a more flexible development mechanism. Because sweater production follows yarn-first logic, mature knitting factories deeply integrate stock service yarn systems. This means buyers can select directly from yarn mills' reserve libraries of hundreds of ready colors, completely bypassing massive fabric dye lot minimums. Through this model, professional sweater factories can easily support very low MOQ orders, helping brands complete sample development and market testing at maximum speed and minimum risk. HS Code Classification & International Trade Compliance The underlying manufacturing process differences between the two ultimately manifest in international customs clearance and tax compliance. In global customs HS Code classification, flat-bed Fully Fashioned sweaters are typically classified directly under HS 6110 (e.g., 6110.20 cotton knitwear or 6110.11 wool knitwear), while cut-and-sew long-sleeve sweatshirts have different sub-classifications based on material and specific construction, directly affecting final import duty calculations. Moreover, in cross-border B2B sourcing, supply chain compliance depth determines trade safety. For the North American market, for example, knit products involve not only USMCA's strict "yarn-forward" rules of origin but must also meet US CPSC's 16 CFR 1610 flammability standard and FTC care labeling requirements. Choosing a sweater manufacturer well-versed in these international trade rules and traceability laws can cut off customs clearance obstruction and violation penalty risks at the source. 6. Conclusion: Which Should Your Brand Choose? When building an apparel brand's product matrix, sweaters and sweatshirts are never an either-or single-choice question—they carry completely different commercial missions. Objectively, if your brand focuses on street sport, high-frequency daily wear, and needs to quickly support base volume through large-area prints and basics, then cut-and-sew sweatshirts are undoubtedly the most efficient choice. However, when your brand evolves to need distinctive character, hopes to present premiumness through complex physical textures, or plans to leverage zero-waste production to lift retail premiumness—flat-bed knitted sweaters become your core weapon for breaking through homogeneous competition. If you're planning a premium knitwear collection for next season and want to utilize GRS certified recycled yarns and 2G to 18G Fully Fashioned computerized flat-bed technology for complex structural designs—as a specialized sweater manufacturer deeply rooted in B2B, we're ready to provide substantive supply chain support, from sending stock service yarn color cards for material evaluation to executing efficient sample development.
view more