
Party Christmas Trees Knits Custom Sweater Jumpers OEM Factory


- Model Number:USP50005
- Brand Name:JM
- Product Type:Sweater
- Age Group:Children
- Supply Type::OEM Service
- Material:Wool / Acrylic
- Age:Suitable for all
- Gender:Unisex
- Season:Winter
- Sleeve:Long sleeves
- Colors:Red
- Size:Any size
- Design:Christmas Knitting clothing
- Sample Time:Within 7 work days
- Package:As your requested
- Delivery time:Within 15-45 days
- Type:Pullover Sweater
- Supply Ability:400000 Piece/Pieces per Month
- Port:Huangpu, Guangzhou,Shenzhen,Ningbo,Shanghai
- Payment Terms:L/C,T/T,Western Union,PayPal
- Min.Order Quantity:300 Piece/Pieces Let me know your quantity freely
- Price Range:$7 – $10.5 USD

|
Material |
Cotton, Nylon, Polyester etc. (According to customer's requirement.) |
|
Color |
All colors are available |
|
Size |
Can make as your requested |
|
MOQ |
300 pcs |
|
Needle |
1.5/3/5/7/9/12/14/16 can be choose |
|
Lable |
As your requested |
|
Service |
Accept OEM/ODM services |
|
Port |
Huangpu Port, Guangzhou,Shenzhen,Ningbo,Shanghai |
|
Delivery Time |
About 15-45days after get your payment |
|
Package |
Plastic bag; Carton Size: 60*40*30cm (according to your requirement) |
|
Payment |
Paypal ,T/T, Western Union(30%-50% deposite,the balance should be paid before delivery) |
|
Sample |
1. Sample price: according to your design,sample fee will refund to you when you make the order. 2. Samples time: about 3-7 days can be finished. |
Picture show:


1. Empty the sweater pocket prevent the deformation.
2. Hanging clothes: Use appropriate hangers hanging the sweater in a cool, ventilated place, hung for a while, let it to remove the wrinkles.
3. Brush away the dust on the surface of the sweater, the dust if on the sweater for a long time will become a stain, and the dust will affect the appearance of the sweater, can use the cold water to clean, and then blot it with a clean piece of the sweater, but can not use the tissue.
4. If your sweater is wet, and you want to put it to dry immediately, noted can not contact with heat source directly, like in front of the fire roasted, spread out on the electric heater or bask in the big sun. Unless have mention in washing label, can not use dryer to dry it.
5. Not recommend wear the same sweater consecutive 2 days, should give the sweater have enough time to restore its natural elasticity.
6. If you want to stored the sweater for a long time, should wash and dry first.
7. Insect-resistant eat by moth of the sweater is also very important, the commonly used method is the fumigation, it need to be in a sealed container.
8. Preferred dry cleaning or washed by hand, the water temperature, does not exceed 30℃,kind advised choose a special sweater washing liquid.


Related Products

Simple Knitted O-Neck Woolen Custom Sweater Pattern Designs For Men Apparel Supplier OEM

OEM 7GG Computer Knitted Pullover Sweater Pure Cotton Cashmere Custom Letters Crew Neck For Men Manufacturer
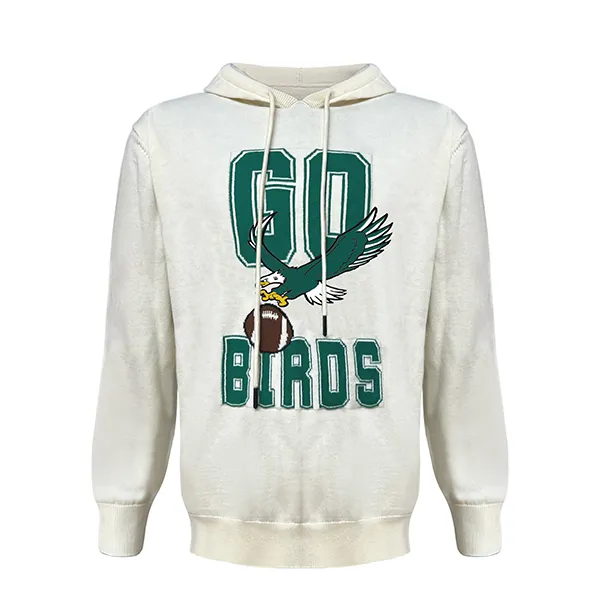
Varsity Football Graphic Print Long Sleeve Pullover Hoodie with Drawstring Hood and Ribbed Cuffs Hem OEM Manufacturer
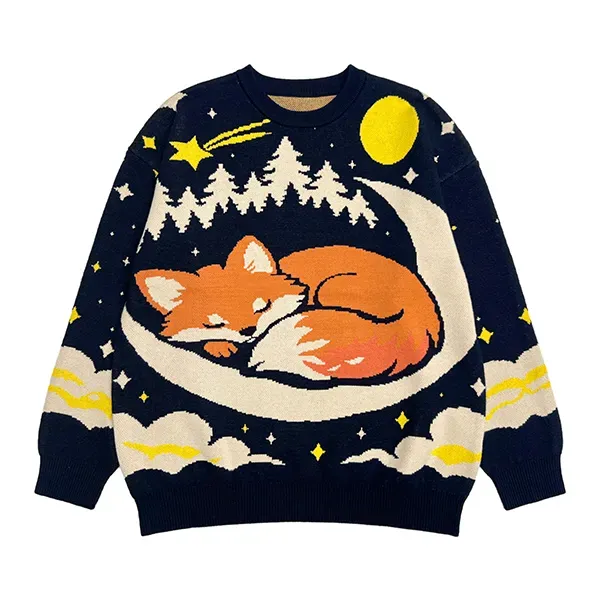
Refined Intarsia Scenic Knitwear from Premium Manufacturer: Custom Sleeping Fox Graphic Pullover
We can customize sweaters of various categories.
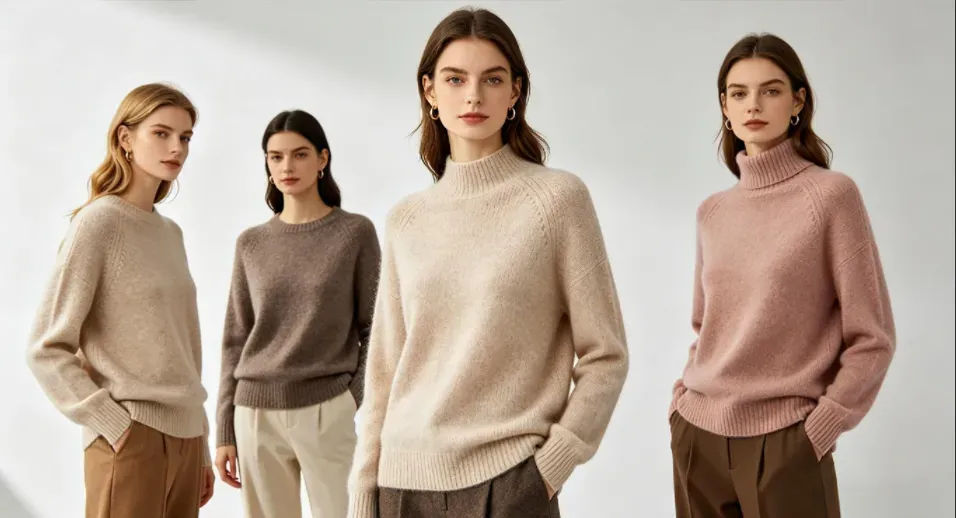
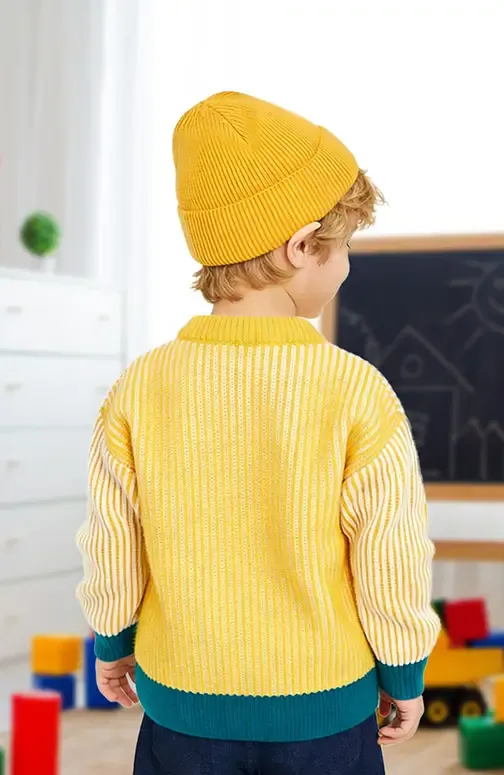
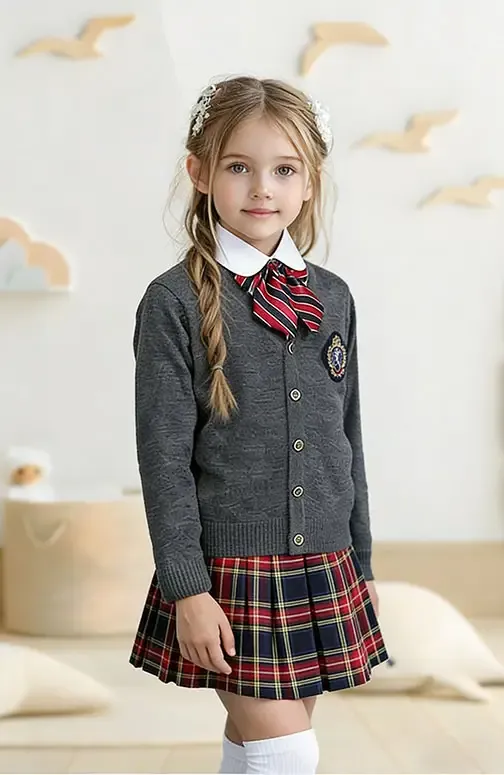
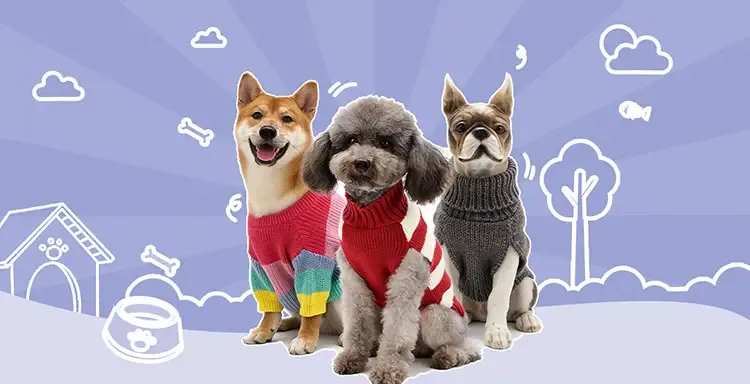

Sweater Factory Video
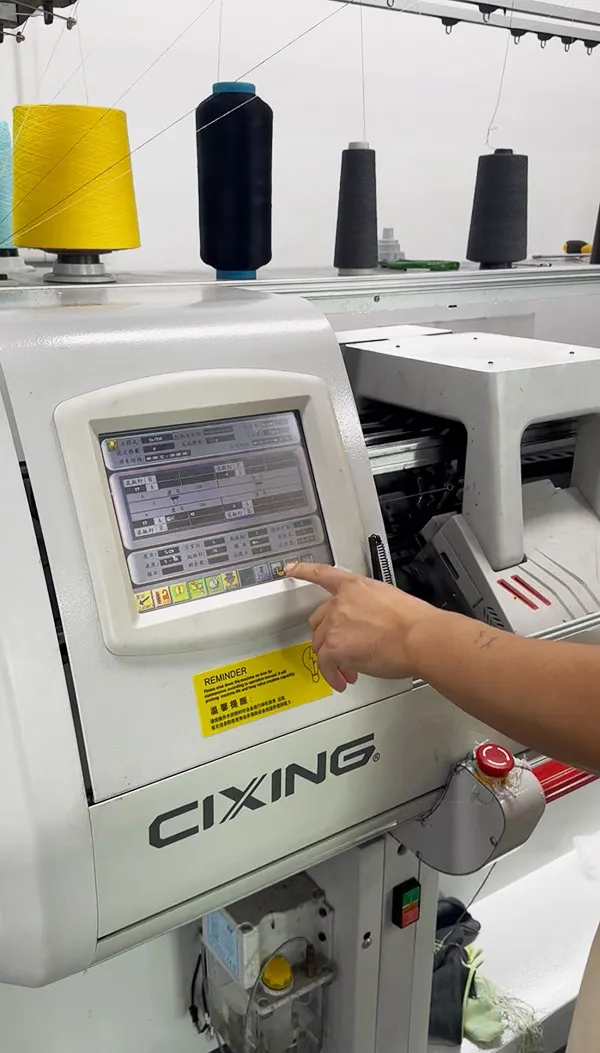
Sweater Manufacturer Sample Room: OEM/ODM Sampling, Pattern Making & Knitting Programming
Duration: 29sUpdated: September 23rd, 2026A detailed walkthrough of our knitwear sample room, showcasing how a professional Private Label Sweaters Manufacturer manages the complete development cycle from client tech pack interpretation to finished prototype approval. The video highlights skilled technicians creating computerized flat knitting programs on German STOLL and Japanese Shima Seiki software, alongside patternmakers calculating stitch density, yarn tension, and shrinkage allowances. Key sampling operations featured include automated panel knitting across 3G, 5G, 7G, 12G, and 14G gauges, precision hand-linking for seamless collar and shoulder joining, manual thread trimming, and steam framing for dimensional stability. Designed to support B2B buyers and fashion designers, this sample development center handles custom proto samples, fit samples, color lab dips, and pre-production samples (PPS) utilizing organic cotton, merino wool, fine cashmere blends, and recycled yarns.
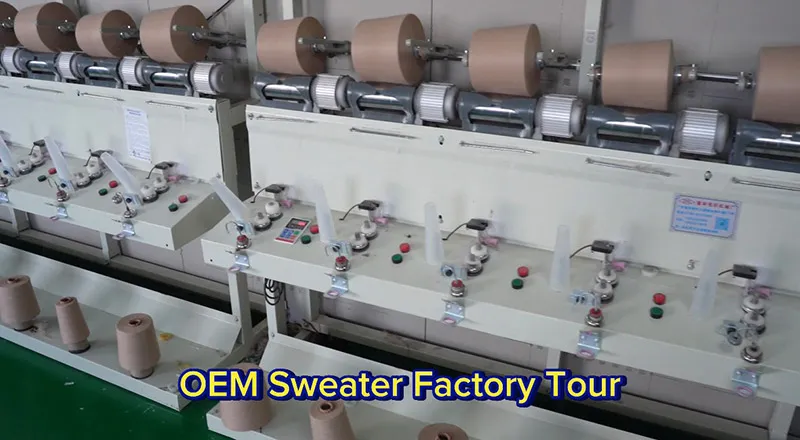
Inside a Leading Knitwear Manufacturer in China – Factory Tour & Behind the Scenes
Duration: 58sUpdated: August 10th, 2026Welcome to our knitwear manufacturing facility in Guangzhou, China. This video takes you behind the scenes of our 3,000-square-meter factory, where we produce high-quality knitted garments for brands worldwide. As a leading sweater manufacturer in China, we specialize in custom OEM and ODM production across five core categories: men's knitwear, women's knitwear, children's knitwear, pet knitwear, and a full range of knitwear accessories. Men's Knitwear & Women's Knitwear Our factory is equipped with over 110 advanced STOLL computerized flat-knitting machines, capable of producing everything from classic crewneck sweaters and V-neck pullovers to fashion-forward cardigans and knit tops for men and women. With a gauge range of 1.5GG to 18GG, we can handle chunky cable knits as well as fine-gauge lightweight styles. Whether you need a bulk order for a retail chain or a small batch for a startup brand, our flexible production lines ensure consistent quality and on-time delivery. We work closely with fashion brands, wholesalers, and importers across North America, Europe, and Australia, offering full-service support from yarn selection to finished garment inspection. Children's Knitwear & Pet Knitwear Our expertise extends to children's knitwear and pet knitwear – two fast-growing segments in the global apparel market. For kids, we produce soft, durable, and safe sweaters in a wide range of colors and styles, from school uniforms to casual wear. All children's garments are crafted from certified materials that meet international safety standards. For pets, we are a trusted manufacturer of custom dog and cat sweaters, offering breed-specific sizing, premium yarns, and creative designs that keep pets warm and stylish. Whether you are launching a pet apparel line or expanding your children's collection, our low MOQ and fast sampling service make it easy to get started. Knitwear Accessories Beyond sweaters, we are also a leading manufacturer of knitwear accessories – including beanies, scarves, gloves, headbands, and knit hats. These accessories are produced using the same high-quality yarns and precision knitting techniques as our garments, ensuring a cohesive look and feel across your entire product line. With our in-house design team, we can develop custom patterns, colors, and branding elements to match your collection's aesthetic. Behind the Scenes: Our Process In this video, you will see every stage of our production process – from yarn intake and quality inspection to computerized knitting, linking, washing, and final quality control. Our facility is certified under GRS, BSCI, WRAP, ISO 9001, and OEKO-TEX, reflecting our commitment to ethical manufacturing and environmental responsibility. We also maintain a dedicated sample showroom where clients can review fabric swatches, gauge samples, and finished prototypes before placing bulk orders. Why Choose Us? As a direct knitwear manufacturer in China, we offer factory-direct pricing, transparent communication, and a dedicated account management team for every project. Whether you need men's knitwear, women's knitwear, children's knitwear, pet knitwear, or knitwear accessories, we are your one-stop partner for reliable, high-quality production. Book Your Factory Tour Today We welcome international buyers to visit our factory and see our operations firsthand. Schedule a visit to meet our team, review our capabilities, and discuss your next collection. Contact us now to arrange your factory tour!
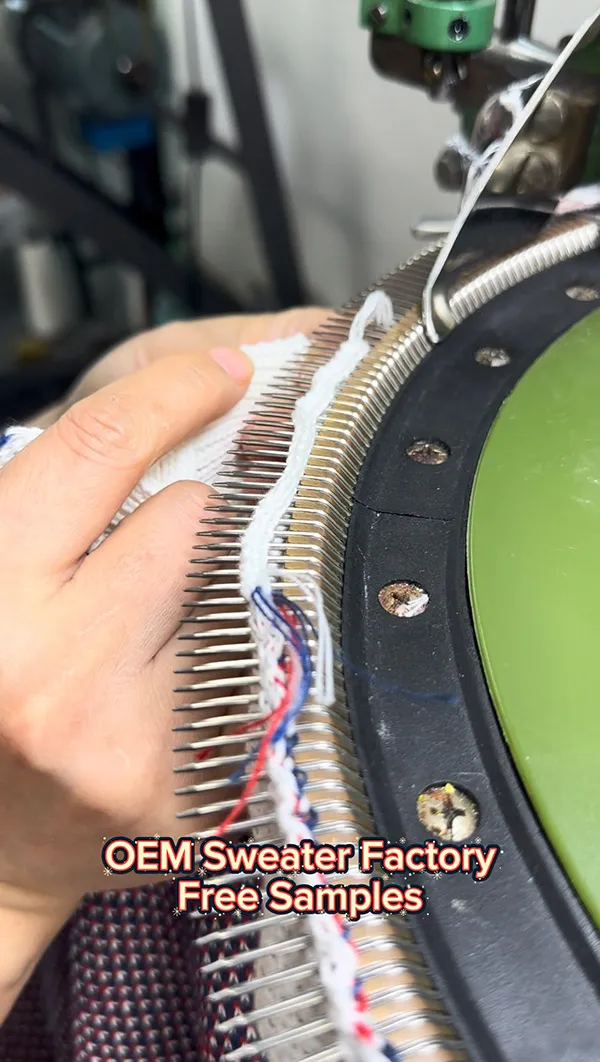
Custom Pullover Sweater: White Striped Ribbed Collar Linking Video Highlights Flat Seams and Free Sample Options
Duration: 21sUpdated: October 7th, 2026This custom pullover sweater video demonstrates how flat, clean seams are assembled for classic crewneck jumpers featuring red, white, and blue striped rib collar trims. Crafted from soft cotton or fine wool blend yarns, the elastic ribbed collar provides comfortable stretch recovery, shape retention, and a neat neckline fit. The timeless contrast tipping style adds a sporty preppy aesthetic, making it an ideal choice for casual daily wear, university streetwear, and collegiate fashion collections. Designed for independent clothing brands, our direct factory setup delivers full OEM/ODM manufacturing for every custom pullover sweater line. We offer flexible low MOQ orders, custom yarn color dye matching, private woven label integration, and free physical samples so design teams can evaluate fabric softness, weight, and seam strength before placing bulk wholesale orders.
Sweater Manufacturer Blog
Knitwear Quality Control: Complete Sweater Inspection Guide
Subtitle:Sweater Manufacturer AQL 2.5, Torquing Prevention, Gauge‑Specific Checks, and Tolerances That Hold Up on the Measuring Table In cross-border knitwear sourcing and custom production, your Quality Control (QC) setup isn't just an inspection checkpoint—it’s the single biggest factor dictating your brand’s margin and survival. Unlike standard wovens, fully-fashioned knits are built loop by loop. Variable yarn tension, moisture regain, unpredictable relaxation shrinkage, and complex panel linking make knitwear inherently dynamic on the factory floor. Over the years, as a professional sweater manufacturer I’ve seen too many brands watch their profits burn over preventable finishing errors: distorted necklines, twisted side seams, premature pilling, or a dropped loop that unravels an entire panel in transit. Left unchecked at the mill, these micro-defects land squarely on the retail side—driving up return rates, damaging retailer relationships, and triggering costly chargebacks. To protect your shipments, we’ve broken down our factory-floor inspection framework into a practical playbook for international sourcing directors, technical designers, and buyers. Below is a breakdown of the core operational protocols covered in this guide: Why standard woven inspections fail on knitwear: How yarn mechanics, gauge tension, and structural elasticity force a completely different inspection approach. The five defects that actually cost you money – and how we stop them: Root causes and real-world countermeasures for spiralling, pilling, shading, and open seams before bulk packing. AQL 2.5/4.0 – thresholds that actually get used: A breakdown of sampling sizes, defect classification (Critical, Major, Minor), and pass/fail rules on the measuring table. Gauge-specific checks: 3GG is not 12GG: Tailoring inspection parameters to match the structural risks of coarse-gauge chunkies versus fine-gauge knits. Measurement POMs and the tolerance trap: Practical flat-lay protocols and realistic tolerance sheets that eliminate stretch disputes between buyers and factory QC teams. Tech Pack must-haves + handling third-party inspectors (SGS/ITS/BV): Aligning your spec sheets and factory SOPs to guarantee clean third-party field reports and zero-defect deliveries. Whether you're an established private-label brand scaling up seasonal bulk orders or a sourcing engineer tightening up your supplier quality agreement, this guide outlines the exact protocols needed to de-risk your knitwear supply chain from cone to carton. Why standard woven inspections fail on knitwear If your QC team uses a woven‑garment checklist on sweaters, you’re effectively writing off a percentage of your order before it leaves the factory. Wovens are cut from stable cloth; knits are loops that move. Tension, moisture regain, and yarn twist behave differently on every batch. I’ve personally watched S‑twist yarns wreck a 12GG production run in our Guangzhou facility simply because the steaming cycle wasn’t adjusted for that specific lot. The side seams spiralled so badly we had to pull the whole batch at the lightboard. The structural shift is simple: a broken thread in a woven stays local; a dropped loop in a knit can ladder the entire panel. So we measure different things: Tension & stress release – if the knitting stress isn’t steamed out, the garment shrinks or twists in the first home wash. Moisture regain – batch‑to‑batch humidity changes shift finished dimensions more than most buyers realise. Torquing – unbalanced single‑ply twist creates that ugly spiral effect. You can’t iron it out, and you can’t press it flat. We run three dynamic tests on every style: neck/cuff recovery (stretch it and see if it snaps back), light‑board scanning (every piece, no exceptions), and shade matching under D65/TL84 before linking. That last one catches dye‑lot mismatches that would otherwise only show up after packing. The five defects that actually cost you money – and how we stop them Defect What causes it Our fix on the floor Torquing / seam twist Over‑twisted yarn or uneven steam setting Pre‑knit reaming to relax twist; we slow the feed tension on the machine if the yarn feels tight; high‑temp steam set after knitting Pilling Short‑staple fibres or too much softener in the wash Switch to long‑staple/combed yarn; run a Martindale test at sample stage – if it scores below 3.5, we don’t cut Dropped stitches / holes Worn latch needles or poor linking Daily needle changes; 100% light‑board scan – zero tolerance. One hole, out of the shipment. Shading / dye‑lot variation Different dye batches or unstable vat temp Strict dye‑lot control; we hold back trims and body panels until they’re matched side‑by‑side under the lightbox Wash‑induced shrink No pre‑shrink allowance or mismatched blend rates Build 3‑5% shrink into the knitting programme; wash‑test the pilot sample and adjust before bulk Here’s a dirty little secret that doesn’t make it into the textbooks: some factories over‑stretch the rib during finishing just to hit the chest measurement on the table. That rib snaps back in transit, and suddenly your spec sheet is worthless. We check the relaxed state specifically to catch that – not the stretched number the production line wants to show you. AQL 2.5/4.0 – thresholds that actually get used We run General Inspection Level II for final random inspection. Critical defects are AQL 0 – one broken needle or a missing fibre label and the whole order stops. For a 2,000‑piece order, we pull 125 pieces. If we find 7 Majors and 10 Minors, the batch rolls. If Majors hit 8, we reject it on the spot. No debate. Real‑world classification (knits only): Major – dropped stitch, open linking seam, side‑seam twist >3%, measurement out of spec, obvious shading. Minor – loose thread >1cm inside, misplaced hang‑tag, light press mark. I’ve had third‑party inspectors flag a 2cm length difference on a heavy 5GG cable knit. We stopped the inspection, let that sweater relax flat for the full 24 hours, and re‑measured. It came back within tolerance. They signed the field report. That’s why we always build a relaxation hold into the FRI schedule – and we insist the inspector watches the re‑measure. Gauge‑specific checks: 3GG is not 12GG Coarse (3‑5GG) – gravity is your enemy. We never hang these; we measure after 24 hours flat. Linking strength gets a hard pull test at the shoulder. Mid (7‑9GG) – torquing and rib recovery are the trouble spots. We check side‑seam twist (must be ≤3%) and stretch neck/cuffs to verify snap‑back. If the rib doesn’t return, we add spandex in the next run. Fine (12‑14GG) – micro‑holes and density. 100% lightboard scan; we use a density glass to check courses and wales per inch and hold ±3% across the batch. Measurement POMs and the tolerance trap Never measure straight out of the polybag. That’s a rookie mistake that costs buyers thousands in false chargebacks. Our protocol: flat‑lay for 2‑4 hours (24 hours for coarse gauges), no stretching, non‑stretch steel tape. Core POMs we actually use: Body length – HPS to hem (including rib) Chest width – half measure, 1” below armhole Shoulder – seam to seam Sleeve length – from CB neck to cuff Neck width/depth – at seam and from back neck to front dip Tolerance sheet (by gauge): POM Fine (12‑14GG) Mid (7‑9GG) Coarse (3‑5GG) Heavy texture Body length ±1.0 cm ±1.2 cm ±1.5 cm ±2.0 cm Chest (half) ±0.8 cm ±1.0 cm ±1.5 cm ±1.5 cm Shoulder ±0.8 cm ±1.0 cm ±1.2 cm ±1.5 cm Sleeve ±1.0 cm ±1.2 cm ±1.5 cm ±2.0 cm Neck ±0.5 cm ±0.8 cm ±1.0 cm ±1.0 cm If the yarn has high spandex content, we add 0.3‑0.5cm on horizontal measures – but we flag that in the Tech Pack before production, never after the fact. Tech Pack must‑haves + handling third‑party inspectors (SGS/ITS/BV) Over 40% of disputes we mediate come down to one thing: the Tech Pack doesn’t specify the relaxed state. Yours must include: Yarn blend and count (e.g. 2/28NM) plus dye method Gauge and stitch structure, with a max float‑length limit A clear POM diagram – not just text Pantone reference and light‑source priority (D65 > TL84) Label position, thread spec, and packing details Performance numbers: pilling ≥3.5, colourfastness ≥4, shrink ≤3% For the 3rd‑party inspector: we give them a dedicated table, lightbox, and lightboard. The checklist they use must match the approved PP sample to the letter – no last‑minute tolerance changes. If they flag an out‑of‑spec measurement, our QC lead has the right to stop the process, re‑relax the piece, and re‑measure on the spot. We photograph the disputed point, sign the field report together, and keep a sealed sample for appeal. Final word (straight to the point) Knitwear quality isn’t inspected in at the end – it’s built into the yarn tension, the relaxation time, and the gauge‑specific checkpoints. If your Tech Pack doesn’t already specify the relaxed state and the recovery test, we’ve got a gap to close before we cut a single cone of yarn. If you’re sourcing knitwear and want a partner who runs these protocols daily – and who will flag the risks before they become chargebacks – send your Tech Pack over. Our technical team will give you a no‑cost feasibility read, a tolerance sample to check our finishing standards, and a supply‑chain risk review specific to your next season.
view more
How to Choose a Knitwear Manufacturer: Complete Buyer Checklist
How to Choose a Knitwear Manufacturer: Complete Buyer Checklist A Step-by-Step Sourcing Guide for Brands — Even Without a Tech Pack Sweater Manufacturer demand is rising as the global knitwear market is projected to surpass $1 trillion by 2035, with demand for high-quality sweaters continuing to grow. But for brand founders, capturing this growth isn't easy. Let’s cut the flattery. Finding a sweater factory isn’t about winning a lowball bidding war. In my experience, the cheapest quote usually comes with hidden costs: missed ship dates, inconsistent sizing, pilling after two washes, and a communication blackhole that makes you want to pull your own hair out. Smart sourcing isn’t about price. It’s about finding a manufacturing partner that’s responsive, transparent, and technically competent. Even if you don’t have a technical designer on staff or a fully built-out tech pack, you can screen factories quickly using these four core criteria. Here’s exactly how. 1. Hardware & Process: What’s Actually on the Floor Forget the glossy sales pitch. A factory’s real capability comes down to two things: the knitting machines they run and how they stitch the pieces together. Gauge (GG) Selection & Machine Capability Gauge refers to the number of needles per inch on the knitting bed. Higher GG = finer, lighter fabric. But here’s the catch: a factory needs the native machine for each gauge. You’re looking for STOLL (Germany) or SHIMA SEIKI (Japan) equipment, not knockoffs. Here’s how the gauges break down: Coarse Knit (3GG – 5GG): Heavyweight fall/winter sweaters, cable knits, cardigans. This gauge tests a factory’s tension control on wide-gauge beds. Mid-Gauge (7GG – 9GG): Your bread-and-butter spring/fall styles. This is the volume sweet spot. The key metric here is stitch uniformity across bulk production. Fine & Superfine (12GG – 18GG): Base layers, fine merino, and cashmere blends. This is where the factory’s climate control and finishing processes get scrutinized. Temperature and humidity swings wreck fine-gauge production. Red flag: A factory that claims they can run 7GG on a 12GG machine by "modifying" the settings. That’s a fancy way of saying your sweater will stretch out and lose its shape after one wear. Walk away. The Joining Process: What Determines Garment Durability This is the single biggest differentiator between a premium sweater and fast-fashion garbage. Hand-Linking (Looping): Each stitch from the knitted panels is looped onto a linking machine, one by one. The result? Seams that are flat, elastic, and almost invisible against the skin. This is how you build garments that last. Cut-and-Sew (Overlock): The cheaper, faster route. Panels get cut with scissors and stitched together with an overlock machine. The seams are bulky, have zero give, and will start fraying at the edges after a few wash cycles. Bottom line: if you’re selling a premium product, hand-linking is non-negotiable. If you’re chasing ultra-low cost, just know the trade-offs. 2. Decoding MOQ: How to Test the Waters Without Breaking the Bank Here’s a truth most brand founders learn the hard way: the MOQ bottleneck usually isn’t the factory’s knitting machines. It’s the dye house. Most mills set dye-lot minimums at 100–300 kg per color. That translates to roughly 300–1,000 finished garments, depending on weight. So how do you get started with 100–200 pieces? Stock service yarns. Stock Service vs. Custom Dyeing If you insist on a specific Pantone match, be prepared to pay for custom dyeing—and wait an extra 2–3 weeks for lab dips and strike-offs. But if you’re willing to work from the factory’s stock yarn color cards, everything changes. Criteria Stock Service Yarns Custom Dyeing MOQ Low (100–200 pcs/design) High (300–1,000+ pcs/design) Lead Time Fast (3–7 days for strike-offs) Slow (adds 2–3 weeks for color development) Risk Low—test multiple colors easily High—you’re sitting on leftover yarn Pro tip: When you send your RFQ, ask this exact question: “What’s your MOQ if we use your stock service yarns?” The answer will tell you immediately if they’re set up for agile, small-batch production or if they’re still operating in the old-school volume model. 3. Sampling Without a Tech Pack & Rigorous Quality Control A good OEM/ODM factory is essentially a development partner. They don’t need a perfect tech pack to start working with you. How to Kick Off Sampling Send them any one of these: High-res reference images or sketches—clearly mark the silhouette and pattern details you want. A physical sample garment—this is the gold standard. Even if it’s the wrong fabric or a different brand, they can reverse-engineer the measurements and build a new pattern from it. The Three Critical Samples Before Production Don’t skip these. Each one protects you from expensive mistakes. Knit-down (Yarn Swatch): This is your first sanity check. It confirms the actual yarn hand-feel, the true color, and how the stitch pattern renders. Approve this before the factory cuts a single panel. Proto Sample (First Fit Sample): This is your first look at actual garment silhouette and construction. Check the fit, the drop, the armhole depth. This is where you catch pattern issues. PPS (Pre-Production Sample): This is the non-negotiable gatekeeper. The PPS must be made with 100% production yarn, trims, and finishing processes. That means the same dye lot, the same wash, the same steam-setting. Do not—under any circumstances—authorize bulk production without a signed-off PPS in hand. The Quality Benchmarks That Matter (AQL 2.5) Hold your factory to these three metrics during the final inspection: Size tolerance: Within ±1.5 cm of the spec sheet. Pilling resistance: ISO/AATCC rating of 3–4 or higher. Anything below that and your customers will complain within weeks. Washing shrinkage: Must fall within ±3% to ±5% after the standard wash-and-set finishing process. 4. Sending a Smart RFQ & Spotting Supplier Red Flags You don’t need a novel. You need a concise, information-rich inquiry that gets you a real quote on the first pass. The Four Components of a High-Conversion RFQ Include these four elements, and you’ll get a useful response—not a generic brochure. Estimated quantity: Total pieces AND breakdown per color. (Example: 200 total, 100 pcs in Navy, 100 pcs in Charcoal) Visual reference: Either a high-quality photo or simply state: “Sample garment available for shipping.” Yarn & gauge preferences: Be specific. (Example: “7GG mid-gauge, cotton-blend, using your stock service yarns.”) Target market & delivery deadline: (Example: “US market—must hit warehouse by October 15th.”) Factory Red Flags: Three to Walk Away From I’ve seen these patterns repeat across dozens of factory audits. If you hit any of these, keep looking. Slow sampling response: If they can’t turn a proto sample around on time, they’re telling you—loudly—that they can’t manage production schedules. Bulk will be worse. Pushing custom dyeing exclusively: If they refuse to show you a stock yarn color card and insist on high-MOQ custom dyeing, they don’t have a service model for emerging brands. They’re still hunting whales. No industrial steam-setting equipment: If they’re finishing sweaters with a hand iron instead of a proper steam tunnel or press, your garments will shrink and deform after the customer’s first wash. That’s a chargeback waiting to happen. Final Take: Build a Supply Chain, Not a One-Off Deal Choosing a knitwear factory isn't a transaction. It’s the foundation of your brand’s supply chain. The playbook is simple: Use stock service yarns to de-risk your initial order. Lock down your PPS before bulk production starts. Send a tight, data-driven RFQ to filter out time-wasters. Do that, and you’ll operate like a seasoned sourcing pro—regardless of your team’s size. Ready to Skip the Sourcing Headaches? Finding a knitwear partner who balances flexible MOQs, rigid quality control, and transparent communication shouldn’t feel like a gamble. At JM Sweater (Guangzhou Junma Apparel Co., Ltd.), we’ve spent 21 years perfecting custom knitwear manufacturing for growing global brands. With a 3,000 m² facility and annual capacity of 1.2M garments, we bridge the gap between high-end craftsmanship and flexible production—whether you need low-MOQ stock yarn development or full-scale OEM/ODM runs. Need help reviewing a Tech Pack or calculating yarn yield? [Get a Free Production Assessment & Quote within 24 Hours]
view more
Italian Knitwear Trends for AW Yarns, Silhouettes, and Stitch Innovations
Table of Contents 1. Executive Summary: The Evolution of Italian Knitwear 2. YARNS & FIBERS: Material Innovations in A/W Italian Collections 3. STITCH INNOVATIONS & STRUCTURES: Engineering 3D Texture 4. SILHOUETTES & TAILORING: Fluidity Meets Architectural Volume 5. B2B OEM/ODM BRIDGING: Translating Italian Design into Scalable Production 6. Frequently Asked Questions (FAQs) – Sourcing & Technical Insights 7. Conclusion & Actionable Call to Action 1. Executive Summary: The Evolution of Italian Knitwear The latest signals coming out of Pitti Filati, Pitti Uomo, and Milan Fashion Week point to a marked shift in autumn winter knitwear design across Italy. The market has moved well beyond the restrained "Quiet Luxury" vocabulary that dominated recent seasons. What buyers and designers are chasing now is tactile luxury — an approach that foregrounds extreme surface hand-feel and artisanal stitch engineering. Plain jersey is no longer enough. Long-hair mohair, raised 3D jacquard, and seamless whole-garment construction are driving the kind of rich texture and visual depth that retail buyers want on the shelf. That said, translating this distinctly Italian aesthetic into commercially viable, scalable product is where brands hit real friction — making the choice of an experienced custom sweater manufacturer critical on the supply chain side. Three bottlenecks come up repeatedly: Yarn cost. Top-tier Italian-spun fibers carry a premium that squeezes margins at scale. Knitting complexity. 3D stitch structures demand machinery capability and operator skill that not every factory has. Yarn waste. High-gauge (12G–18G) knitting combined with shaped panels pushes waste rates up significantly. The way through these barriers is to connect front-end design intent with modern flatbed knitting engineering. By working with the latest Italian knitwear trends A/W directions and mapping them against fully computerized flatbed machines (2G through 18G) and WHOLEGARMENT® 3D seamless technology, brands can hold onto the Italian hand-feel and structural beauty while keeping production costs controlled and output standardized. 2. YARNS & FIBERS: Material Innovations in A/W Italian Collections The soul of Italian autumn winter knitwear lives in the yarn. This season, textile engineers and designers have pushed fiber blending and finishing technology to the limit, drawing maximum tactile and functional performance out of natural materials. 2.1 Tactile & Halo Yarns Long-hair mohair, baby alpaca, and bouclé / terry yarns are the headline act. These yarns get their signature cloud-like halo effect through finishing processes — specifically washing and milling, followed by brushing. In production, we typically run a high-gauge base yarn in the blend. That keeps the structure stable while letting the surface deliver the full tactile experience. 2.2 Sustainable & Certified Fine Wools Sustainability is no longer a nice-to-have — it's a core procurement metric. This season's Italian yarn direction leans heavily on three certification and performance benchmarks: GRS-certified recycled cashmere. Combines a strong sustainability narrative with cost efficiency. Paired with a sustainable cashmere yarn supplier's traceability system, it brings raw material costs down substantially. RWS merino wool. Guarantees animal welfare and fiber traceability — the foundation for any credible RWS merino wool knitwear program. Basolan-treated wool. A micro-scale shrink-resist process that preserves wool's natural elasticity and warmth while adding machine-washability and anti-pilling performance. Beyond certifications, undyed neutrals and mélange yarns are showing up across collections. These reduce the chemical load of dyeing while giving knitwear a refined, naturally derived color palette. 2.3 Metallic Accents & Silk Blends For a subtle touch of luxury in everyday wear, designers are specifying Lurex and silk-cashmere blends. Using plating techniques, the faint metallic or silk sheen flickers in and out of the stitch structure — adding visual layering without shouting. Italian Yarn Characteristics vs. B2B Sourcing Alternatives Matrix Yarn Type Warmth Pilling Resistance Raw Cost Production MOQ Typical Application Virgin Cashmere Very High (5/5) Moderate (3/5) Very High ($$$$$) High Luxury turtlenecks, minimal cardigans GRS Recycled Cashmere High (4/5) Moderate (3/5) Moderate ($$$) Flexible Sustainable accessible luxury, eco basics RWS Merino High (4/5) Good (4/5) Moderate ($$$) Low Business knitwear, fine-gauge base layers Mohair Bouclé Medium-High (3.5/5) Low (2.5/5) Medium-High ($$$$) Moderate Voluminous outerwear, mohair boucle sweater OEM As a manufacturing partner focused on premium knitwear export, we maintain long-standing relationships with GRS and OEKO-TEX certified yarn suppliers. That gives brand buyers access to raw material solutions that deliver Italian hand-feel at competitive cost. 3. STITCH INNOVATIONS & STRUCTURES: Engineering 3D Texture In Italian autumn winter knitwear design, stitch structure is what gives a garment three-dimensionality and body. Modern computerized flatbed technology has freed designers from the constraints of plain jersey and basic rib. Through precise stitch engineering, artisanal handwork can now be translated into efficient, repeatable industrial production. 3.1 Raised 3D Jacquard & Modern Intarsia This season's jacquard and intarsia have moved past the flat, printed look: Double-bed 3D raised jacquard. By controlling needle bed alignment on a double-bed machine, the face shows a raised, sculptural motif while the reverse forms a clean, organized backing. This significantly boosts fabric density and structure. As a specialized 3D jacquard sweater factory, we fine-tune tension during knitting to keep the pattern sharp and eliminate float yarns pulling across the back. Modern color-block intarsia. For abstract geometry and color contrast, dedicated intarsia feeders knit each color zone separately. Unlike traditional jacquard with its float yarns on the reverse, our intarsia panels — as a custom custom intarsia knitwear supplier — come out flat with no bulk on the back. The garment wears lighter and more comfortably. 3.2 Dimensional Cable & Brioche Ribbing Traditional heavy cables eat yarn and weigh a garment down. This season's cable knit structural engineering focuses on balancing "volume" with "lightness": Transfer & tuck stitches. By introducing tuck and transfer stitches at cable twists, we create honeycomb or openwork relief effects. The cable interior fills with air. Brioche ribbing. Combined with high-elasticity rib, this gives the vertical stitch columns a deep, springy, three-dimensional groove — enriching the tactile layering of heavy-gauge sweaters. 3.3 Light-as-Air Openwork & Pointelle Openwork also shines in autumn winter. Through precise transfer pointelle on computerized flatbed machines, paired with mohair or fine-gauge merino, we achieve a vintage lace effect that mimics hand crochet — crochet-look machine stitches. This preserves warmth while adding visual breathability for layering. 3.4 3D WHOLEGARMENT® & Complete Garment For brands chasing the ultimate wearing experience and clean silhouette, whole-garment seamless knitting represents the premium manufacturing standard: Zero-waste knitting. The entire garment is knitted in one piece, in three dimensions, on the machine. No cutting. No linking. This dramatically reduces waste rates on expensive yarns like cashmere and fine wool. Seamless fit. A whole garment 3D seamless sweater eliminates shoulder and side seams entirely — no friction, no pull. The garment follows the body's curves like a second skin, aligning with the Italian emphasis on fluidity and comfort. 4. SILHOUETTES & TAILORING: Fluidity Meets Architectural Volume Autumn winter Italian knitwear silhouettes are merging fluidity with architectural volume. This season's cuts break away from the loose, formless feel of traditional sweaters. Through precise garment construction, knitwear now achieves a structured outline that rivals tailored suiting. 4.1 Architectural Milano-Knit Outerwear Dense Milano stitch has become the core technique for this season's knit outerwear: Structural support. Milano stitch uses a double-face, high-density knit with excellent tensile resistance and body. Used in double-breasted coats or heavy overcoats, it creates a boxy silhouette with the tailored feel of woven cloth — tailored knitwear in the truest sense. Manufacturing precision. As an experienced milano stitch sweater supplier and boxy cardigan OEM manufacturer, we control flatness and shrinkage strictly during finishing. The result: outerwear that holds its architectural lines while retaining knitwear's natural comfort stretch. 4.2 Oversized Funnel Necks & Slouchy Turtlenecks Collar and neckline shapes are the visual anchor this season: Collar scaling and linking. Extra-high funnel necks and draped, foldable necklines require linking with very high elasticity. Drop shoulders and drape. Slanted drop-shoulder construction, paired with lightweight high-gauge yarns, lets the garment form natural drape folds at the shoulder — elegant but relaxed. 4.3 Multi-Layerable Vests, Capes & Sets Layering pieces built for unpredictable weather are having a moment: Knit vests and capes. Deep V-neck vests and seamless capes emphasize edge reinforcement (Mobilon tape structural strengthening) to prevent distortion from repeated layering. Knitwear co-ord sets. Matching tops, bottoms, and scarves require stitch harmony and strict yarn dye-lot control — a production approach that gives premium brands a cohesive, high-margin offering. As a manufacturing partner focused on premium knitwear export, we use precise pattern drafting and linking processes to translate Italian architectural lines into high-quality architectural knitwear coats and premium custom collections. 5. B2B OEM/ODM BRIDGING: Translating Italian Design into Scalable Production For overseas apparel brands, sourcing managers, and independent designers, the biggest challenge in developing an Italian-style knitwear collection is this: how do you achieve controllable production costs and industrial-scale output without sacrificing quality or design detail? As a premium knitwear manufacturing and export partner, we bridge that gap through engineering precision and supply chain management. 5.1 Gauge Precision Matching: 2G to 18G Different gauges determine a sweater's structure and drape. Our production base is equipped with 110 fully computerized flatbed machines, including German STOLL and Japanese Shima Seiki: Coarse gauge (2G / 3G / 5G / 7G): Ideal for hand-knit looks, chunky cables, and rugged outerwear knits. High gauge / fine gauge (12G / 14G / 18G): Built for accessible luxury base layers, premium merino, and ultra-thin cashmere — delivering superior flatness and drape. As a specialized high gauge knitwear factory China, we maintain zero dropped stitches and uniform stitch density at high gauges. 5.2 Cost-Engineering: Practical Optimization Strategies Without compromising the face-side visual, our technical team can deliver actionable custom sweater OEM cost breakdown optimization: Structural optimization. For yarn-heavy 3D cables or complex intarsia, we can engineer the back panel in single jersey or rib while keeping the front in 3D stitch. This directly cuts yarn weight and labor time by 15%–20%. Blend substitution. We recommend using cost-effective core-spun yarns or GRS recycled fibers in the base structure, keeping premium mohair or cashmere on the surface for hand-feel. Raw material budgets drop significantly. 5.3 Washing & Finishing: Hand-Feel Calibration The signature "cloud hand" and loft of Italian knitwear is 70% determined by washing and milling in the finishing stage: Precise water quality and temperature control. We strictly calibrate wash water pH, temperature, and softener ratios. Shrink-resist and anti-pilling. For wool and cashmere, standardized milling and drying time control lets us build a fluffy halo while maintaining pilling resistance and dimensional stability — replicating a hand-feel close to Italian origin. 5.4 Quality Compliance: International Standards & Certifications To ensure smooth customs clearance and retail compliance globally, our production follows strict international testing protocols: QC inspection. Full AQL 2.5 sweater quality inspection — covering seam tensile strength, dimensional tolerances, and stitch defects. Regulatory compliance. Meeting US CPSC flame retardancy testing (16 CFR 1610) and FTC care labeling requirements. All stress points are reinforced with Mobilon elastane tape. Sustainable factory certifications. GRS, OEKO-TEX Standard 100, and BSCI. As a compliant sustainable knitwear manufacturer, we help brands enter European and North American retail channels without friction. 6. Frequently Asked Questions (FAQs) – Sourcing & Technical Insights This section addresses the four most common technical and supply chain questions overseas buyers ask when developing Italian-style knitwear. Q1: Without using 100% imported luxury yarns, how do you achieve Italian-level hand-feel? A: By blending natural wool or cashmere with high-elasticity core-spun yarn, combined with precise washing and milling in finishing. This builds a fluffy halo effect while reducing raw material costs by over 30%. Q2: What is the fundamental difference between 3D WHOLEGARMENT® and traditional cut-and-sew knitwear? A: WHOLEGARMENT® knitting produces the entire garment in one piece, in three dimensions, on the machine. It eliminates shoulder and side seams entirely — no friction against the body — and achieves near-zero-waste production. Q3: What are the sampling lead times and MOQs for complex jacquard and intarsia custom styles? A: After Tech Pack confirmation, sampling takes 7–10 working days. MOQ for in-stock color yarns starts at 100–200 pieces per style. For custom-dyed yarns, MOQ is typically 300–500 pieces per style. Q4: How do you solve pilling on high-gauge (12G–18G) merino and cashmere sweaters? A: By selecting high-twist two-ply yarns, increasing stitch density, and combining with an anti-pilling wash and setting process. Pilling resistance consistently meets ISO Grade 4 or above. 7. Conclusion & Actionable Call to Action The essence of autumn winter Italian knitwear trends lies in the seamless fusion of extreme tactile materials, three-dimensional stitch engineering, and architectural silhouettes. Whether you're a premium brand chasing top-tier hand-feel or a growing designer label focused on cost efficiency, the key to successfully translating Italian aesthetics is choosing a manufacturing partner with genuine stitch engineering capability and rigorous quality standards. We operate a 3,000 sqm modern production facility with 110 fully computerized flatbed machines spanning 2G to 18G, plus 3D seamless WHOLEGARMENT® technology. We provide knitwear OEM/ODM services to global clients, meeting AQL 2.5 inspection standards. Ready to bring Italian hand-feel into your next autumn winter collection? Contact us and submit your Tech Pack or design references. Our technical engineering team will provide a free sampling feasibility assessment, optimal gauge recommendations, and a transparent yarn cost breakdown — within 48 hours. 📩 [Start an Inquiry / Request Sample Development]
view more