
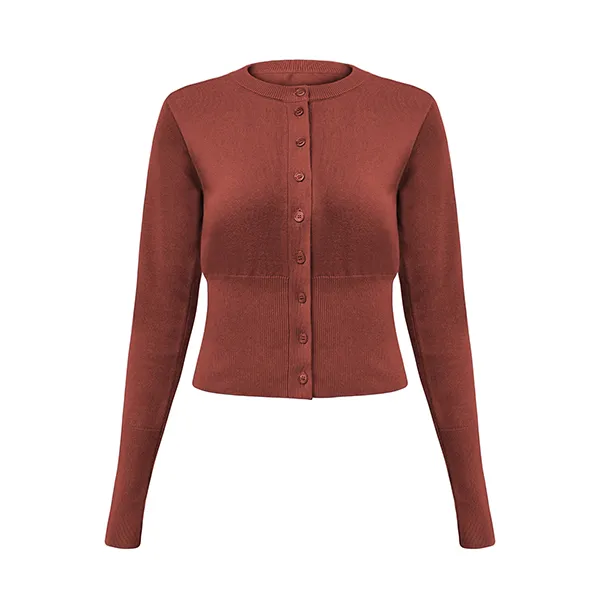
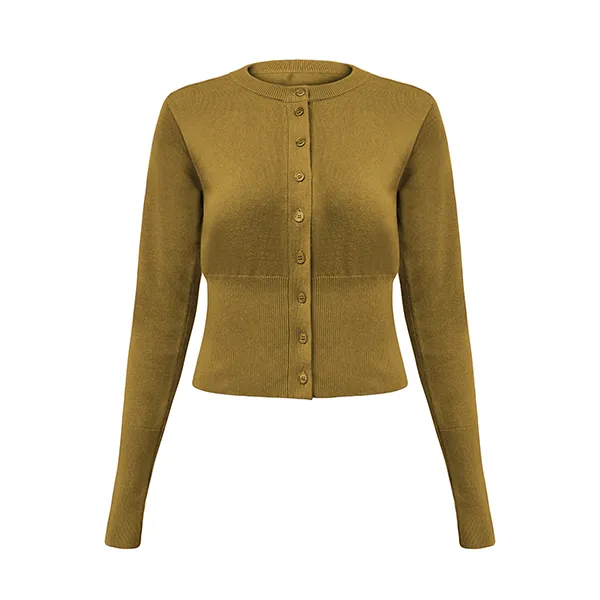
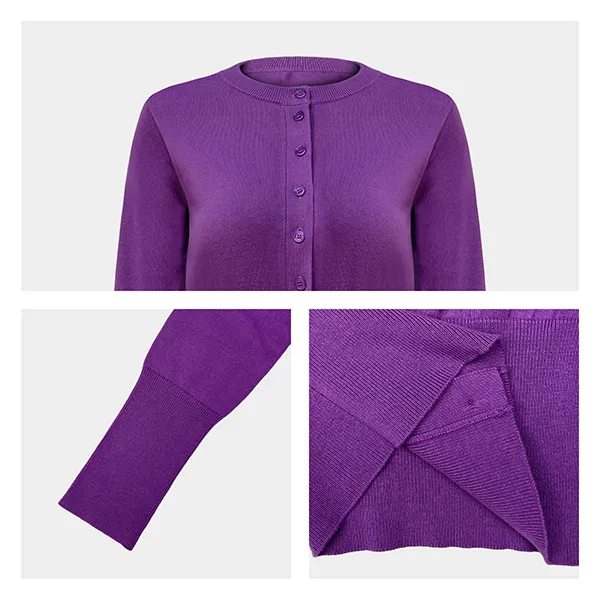
Cropped Crew Neck Button Front Fine Knit Cardigan with OEM Service by Manufacturer and Ribbed Hem
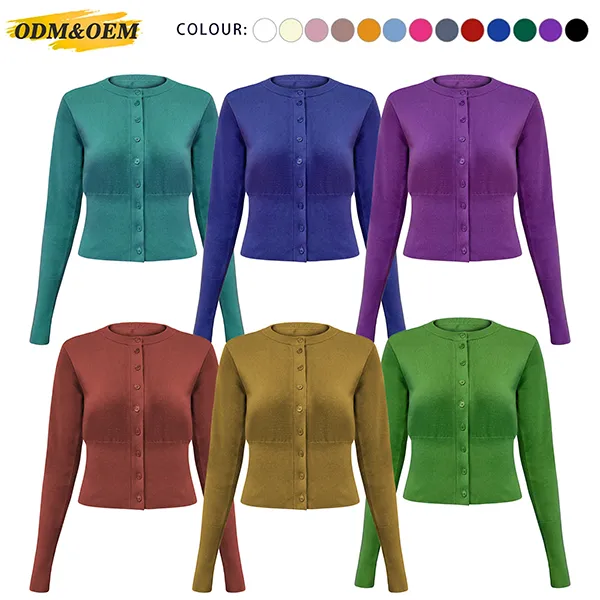
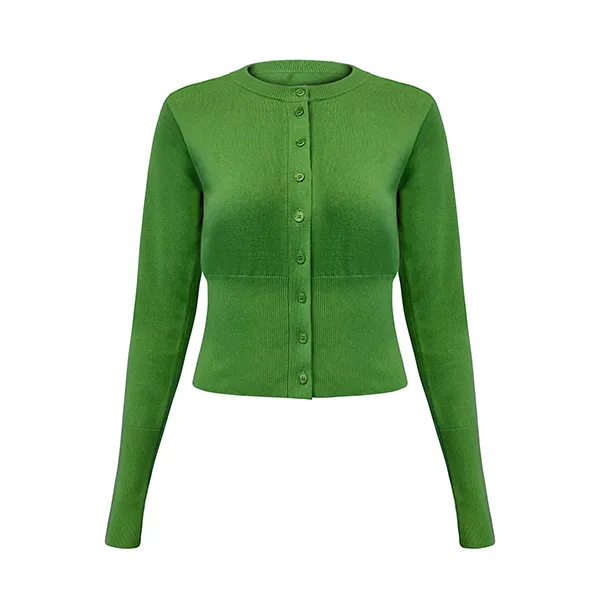
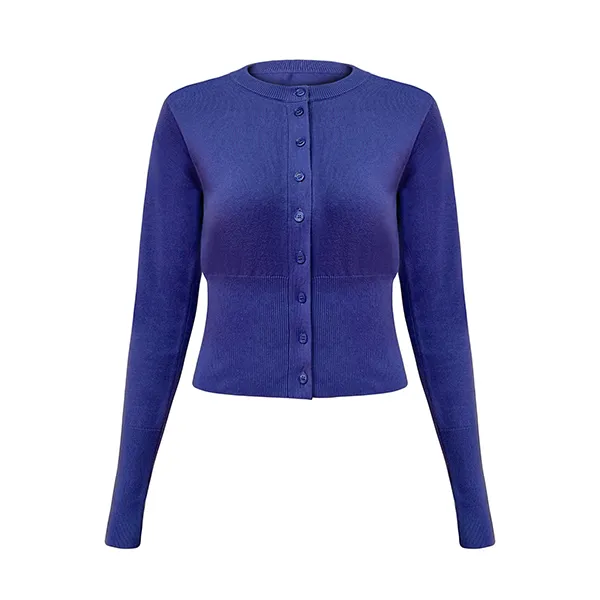
- Product Type:Cardigan Sweater
- Material:Premium cotton, acrylic, wool, viscose, or custom blended yarns.
- Knit Structure:Fine gauge flat knit body with ribbed neck, cuffs, and hemline.
- Target Season:Spring, autumn, and early winter transitional layering wear.
- Design Details:Cropped cut, crew neck, front button placket, and ribbed hems.
- Model Number:JK20250911A
- Size:Adults XS/S/M/L/XL/2XL/3XL or customized
- OEM/ODM:Size,Color,Tag,Printing,Embroidery can be customized
- MOQ:Sample 1pcs,customized products 50pcs
- Sample:Buy samples to check quality, then place bulk orders
- Sample Fees:The sample fee will be returned to you after placing bulk order
- Sample Time:3-7 working days
- Production Time:10-20 working days
- Customized:We produce only original-design knitwear – your own designs or ours.
- Price Range:$12.1 – $18.9 USD
-
Yarn Type & Composition
-
Material Blend: Premium fine-gauge cotton, viscose, acrylic, or customized soft blended yarns. Carefully selected to deliver a smooth, sleek surface texture with a lightweight feel and excellent drape, perfect for a tailored, feminine silhouette.
-
Performance Profile: High-twist fine yarn formulation specifically engineered for edge definition and shape retention, ensuring the flat knit fabric maintains its crisp structure and the short-length hem retains its refined finish after regular wear and gentle laundering.
-
-
Knitting & Technical Craftsmanship
-
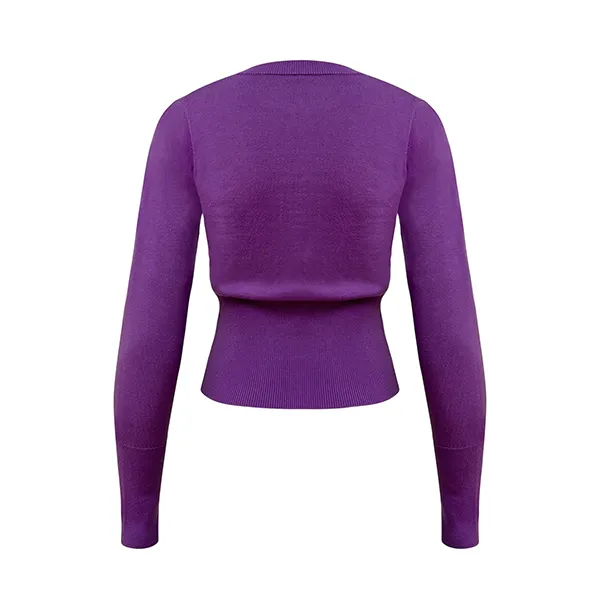
Weave & Pattern Structure: Fine Flat Jersey Knit Body with Contrast Ribbed Waist Panel. Crafted with a smooth, fine-gauge flat knit construction on the upper torso, seamlessly transitioning into a dense, wide-ribbed knit panel at the waist. This structural contrast adds both visual interest and exceptional stretch recovery.
-
Tailoring & Finishing: Features a clean crew neckline, a full-length front button placket with minimal round buttons, elongated long sleeves for a contemporary look, and a wide ribbed bottom hem that perfectly frames the cropped length, delivering a sleek, modern everyday style.
-
-
Support Customization
-
Color Management: Full access to 10,000+ Pantone TPG/TCX color shades for precise, boutique-level color matching on the fine-gauge body and contrasting ribbed waist panel.
-
Sustainable Sourcing: Full support for GRS-certified recycled fibers, BSCI/WRAP-compliant production facilities, and eco-friendly manufacturing protocols.
-
OEM/ODM Flexibility: Complete private-label customization, including custom button styles, woven neck labels, branded hang tags, and individualized retail-ready eco-packaging.
-
-
Seasonal Suitability
-
Target Seasons: Spring, Autumn, and Early Winter Transitional Layering.
-
Market Position: A stylish, minimalist essential ideal for modern casual wardrobes, layered office attire, and versatile daily wear collections.
-
-
Typical Lead Time
-
Prototyping (Sampling): 3 - 7 Working Days. Rapid pattern calibration and express sample dispatch for customized ribbed waist proportions, sleeve length adjustments, and sizing grading.
-
Mass Production: 10 - 20 Working Days. Strictly executed within our certified manufacturing facility to ensure consistent, retail-ready quality control for fine-gauge cropped knitwear.
-
-
Manufacturing Advantage
-
Backed by 21 years of manufacturing heritage as a specialized knitwear Manufacturer, we are highly skilled at crafting fitted cropped cardigans with seamless body-to-rib transitions and precise button alignments. Our dedicated quality assurance team conducts stringent checks on fabric tension and edge finishing, ensuring that every OEM order consistently meets rigorous international retail compliance standards for structural elegance and long-term durability.
-
Related Products
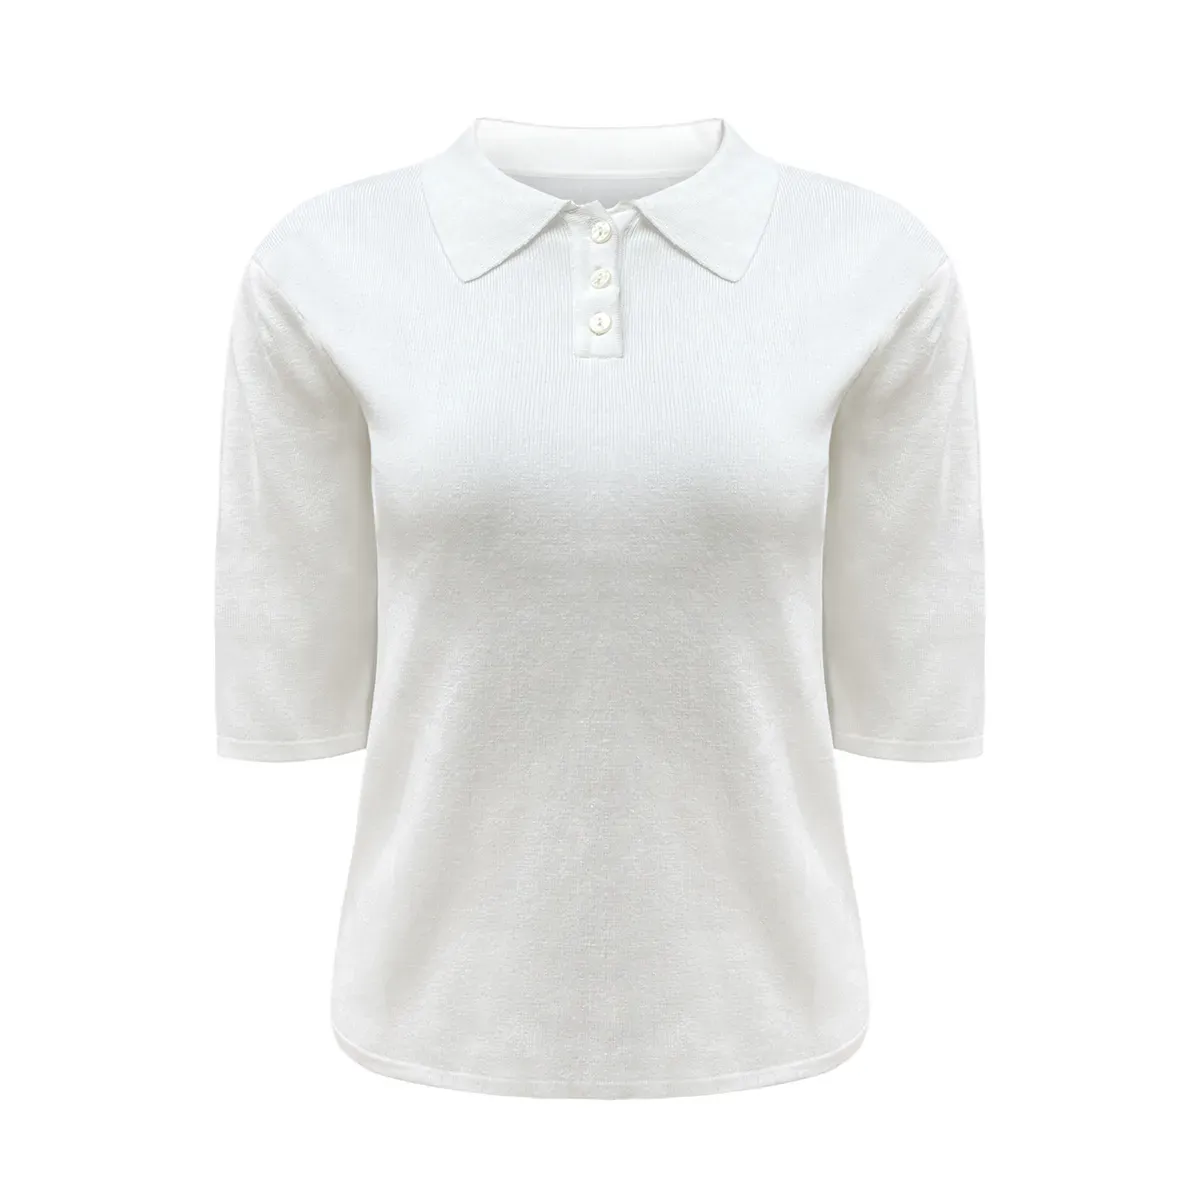
Custom Vintage Polo Jumper from Premium Manufacturer: Half-Sleeve Jersey Knit Three-Button Retro Slim Fit Sweater

Spring Summer Short Sleeve Wool Knitted Sweater Dress Custom For Women OEM Supplier
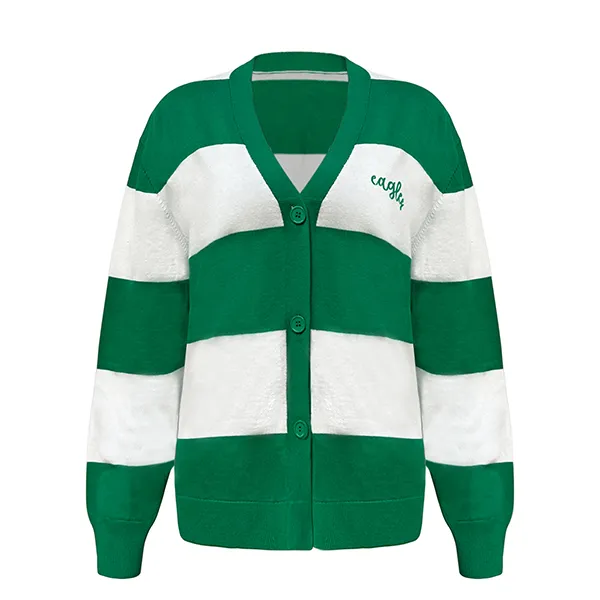
Colorblocked Striped Knit V-Neck Cardigan OEM Button Front Sweater Manufacturer Relaxed Drop Shoulder Casual Jumper

OEM Cropped Hoodie from Manufacturer: Contrast Lined Zip-Up Cardigan with Ribbon Detail & Long Ribbed Cuffs
We can customize sweaters of various categories.

Sweater Factory Video
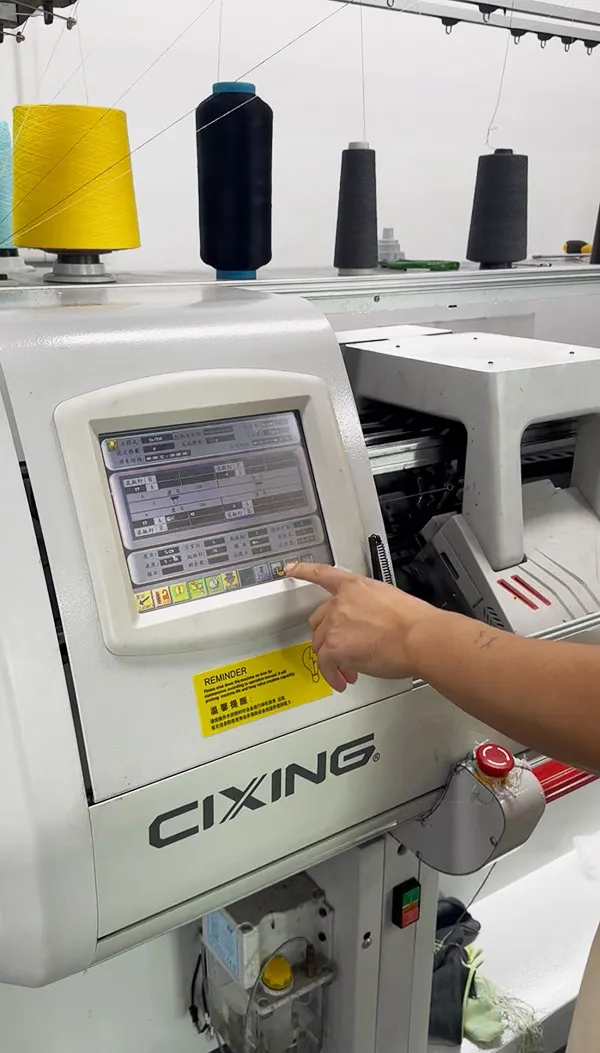
Sweater Manufacturer Sample Room: OEM/ODM Sampling, Pattern Making & Knitting Programming
Duration: 29sUpdated: September 23rd, 2026A detailed walkthrough of our knitwear sample room, showcasing how a professional Private Label Sweaters Manufacturer manages the complete development cycle from client tech pack interpretation to finished prototype approval. The video highlights skilled technicians creating computerized flat knitting programs on German STOLL and Japanese Shima Seiki software, alongside patternmakers calculating stitch density, yarn tension, and shrinkage allowances. Key sampling operations featured include automated panel knitting across 3G, 5G, 7G, 12G, and 14G gauges, precision hand-linking for seamless collar and shoulder joining, manual thread trimming, and steam framing for dimensional stability. Designed to support B2B buyers and fashion designers, this sample development center handles custom proto samples, fit samples, color lab dips, and pre-production samples (PPS) utilizing organic cotton, merino wool, fine cashmere blends, and recycled yarns.
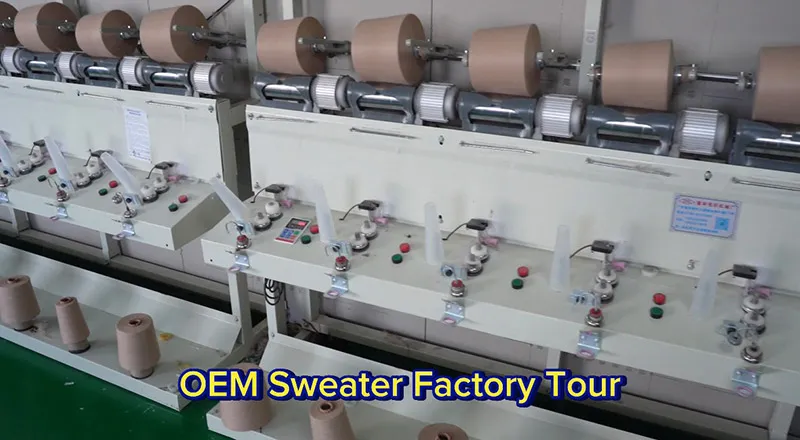
Inside a Leading Knitwear Manufacturer in China – Factory Tour & Behind the Scenes
Duration: 58sUpdated: August 10th, 2026Welcome to our knitwear manufacturing facility in Guangzhou, China. This video takes you behind the scenes of our 3,000-square-meter factory, where we produce high-quality knitted garments for brands worldwide. As a leading sweater manufacturer in China, we specialize in custom OEM and ODM production across five core categories: men's knitwear, women's knitwear, children's knitwear, pet knitwear, and a full range of knitwear accessories. Men's Knitwear & Women's Knitwear Our factory is equipped with over 110 advanced STOLL computerized flat-knitting machines, capable of producing everything from classic crewneck sweaters and V-neck pullovers to fashion-forward cardigans and knit tops for men and women. With a gauge range of 1.5GG to 18GG, we can handle chunky cable knits as well as fine-gauge lightweight styles. Whether you need a bulk order for a retail chain or a small batch for a startup brand, our flexible production lines ensure consistent quality and on-time delivery. We work closely with fashion brands, wholesalers, and importers across North America, Europe, and Australia, offering full-service support from yarn selection to finished garment inspection. Children's Knitwear & Pet Knitwear Our expertise extends to children's knitwear and pet knitwear – two fast-growing segments in the global apparel market. For kids, we produce soft, durable, and safe sweaters in a wide range of colors and styles, from school uniforms to casual wear. All children's garments are crafted from certified materials that meet international safety standards. For pets, we are a trusted manufacturer of custom dog and cat sweaters, offering breed-specific sizing, premium yarns, and creative designs that keep pets warm and stylish. Whether you are launching a pet apparel line or expanding your children's collection, our low MOQ and fast sampling service make it easy to get started. Knitwear Accessories Beyond sweaters, we are also a leading manufacturer of knitwear accessories – including beanies, scarves, gloves, headbands, and knit hats. These accessories are produced using the same high-quality yarns and precision knitting techniques as our garments, ensuring a cohesive look and feel across your entire product line. With our in-house design team, we can develop custom patterns, colors, and branding elements to match your collection's aesthetic. Behind the Scenes: Our Process In this video, you will see every stage of our production process – from yarn intake and quality inspection to computerized knitting, linking, washing, and final quality control. Our facility is certified under GRS, BSCI, WRAP, ISO 9001, and OEKO-TEX, reflecting our commitment to ethical manufacturing and environmental responsibility. We also maintain a dedicated sample showroom where clients can review fabric swatches, gauge samples, and finished prototypes before placing bulk orders. Why Choose Us? As a direct knitwear manufacturer in China, we offer factory-direct pricing, transparent communication, and a dedicated account management team for every project. Whether you need men's knitwear, women's knitwear, children's knitwear, pet knitwear, or knitwear accessories, we are your one-stop partner for reliable, high-quality production. Book Your Factory Tour Today We welcome international buyers to visit our factory and see our operations firsthand. Schedule a visit to meet our team, review our capabilities, and discuss your next collection. Contact us now to arrange your factory tour!
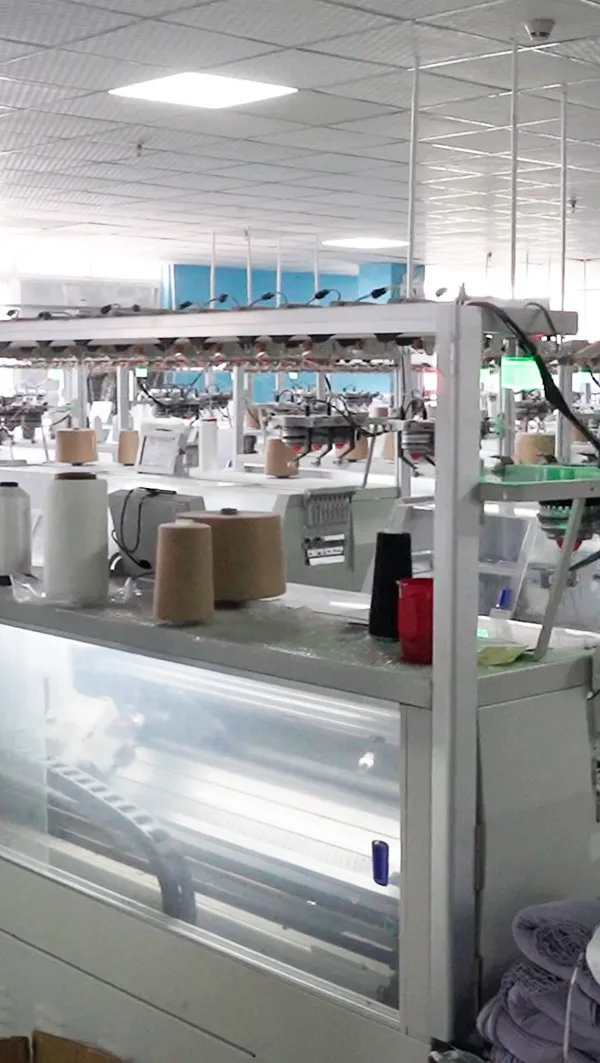
JM Sweater Factory Tour: OEM/ODM Knitting Manufacturing, STOLL Machines & Quality Control in Cotton, Wool & Cashmere
Duration: 27sUpdated: September 23rd, 2026A detailed factory tour video demonstrating the complete OEM sweater manufacturing process, from raw yarn preparation to finished garment packing. The footage captures automated flat knitting machine operations using German STOLL and Japanese Shima Seiki technology across various gauges, including fine 12G/14G and heavy 3G/5G knit structures. Key production stages featured include precise panel knitting, manual hand-linking and collar joining, seam reinforcement with Mobilon tape, sample thread trimming, and industrial steam pressing. Every step incorporates rigorous quality control checkpoints, including needle detector safety scans and dimensional tolerance inspections. Ideal for private label clothing brands, corporate apparel buyers, and distributors, this overview highlights manufacturing capabilities in processing organic cotton, merino wool, cashmere blends, and recycled sustainable yarns.
Sweater Manufacturer Blog
Knitwear Quality Control: Complete Sweater Inspection Guide
Subtitle:Sweater Manufacturer AQL 2.5, Torquing Prevention, Gauge‑Specific Checks, and Tolerances That Hold Up on the Measuring Table In cross-border knitwear sourcing and custom production, your Quality Control (QC) setup isn't just an inspection checkpoint—it’s the single biggest factor dictating your brand’s margin and survival. Unlike standard wovens, fully-fashioned knits are built loop by loop. Variable yarn tension, moisture regain, unpredictable relaxation shrinkage, and complex panel linking make knitwear inherently dynamic on the factory floor. Over the years, as a professional sweater manufacturer I’ve seen too many brands watch their profits burn over preventable finishing errors: distorted necklines, twisted side seams, premature pilling, or a dropped loop that unravels an entire panel in transit. Left unchecked at the mill, these micro-defects land squarely on the retail side—driving up return rates, damaging retailer relationships, and triggering costly chargebacks. To protect your shipments, we’ve broken down our factory-floor inspection framework into a practical playbook for international sourcing directors, technical designers, and buyers. Below is a breakdown of the core operational protocols covered in this guide: Why standard woven inspections fail on knitwear: How yarn mechanics, gauge tension, and structural elasticity force a completely different inspection approach. The five defects that actually cost you money – and how we stop them: Root causes and real-world countermeasures for spiralling, pilling, shading, and open seams before bulk packing. AQL 2.5/4.0 – thresholds that actually get used: A breakdown of sampling sizes, defect classification (Critical, Major, Minor), and pass/fail rules on the measuring table. Gauge-specific checks: 3GG is not 12GG: Tailoring inspection parameters to match the structural risks of coarse-gauge chunkies versus fine-gauge knits. Measurement POMs and the tolerance trap: Practical flat-lay protocols and realistic tolerance sheets that eliminate stretch disputes between buyers and factory QC teams. Tech Pack must-haves + handling third-party inspectors (SGS/ITS/BV): Aligning your spec sheets and factory SOPs to guarantee clean third-party field reports and zero-defect deliveries. Whether you're an established private-label brand scaling up seasonal bulk orders or a sourcing engineer tightening up your supplier quality agreement, this guide outlines the exact protocols needed to de-risk your knitwear supply chain from cone to carton. Why standard woven inspections fail on knitwear If your QC team uses a woven‑garment checklist on sweaters, you’re effectively writing off a percentage of your order before it leaves the factory. Wovens are cut from stable cloth; knits are loops that move. Tension, moisture regain, and yarn twist behave differently on every batch. I’ve personally watched S‑twist yarns wreck a 12GG production run in our Guangzhou facility simply because the steaming cycle wasn’t adjusted for that specific lot. The side seams spiralled so badly we had to pull the whole batch at the lightboard. The structural shift is simple: a broken thread in a woven stays local; a dropped loop in a knit can ladder the entire panel. So we measure different things: Tension & stress release – if the knitting stress isn’t steamed out, the garment shrinks or twists in the first home wash. Moisture regain – batch‑to‑batch humidity changes shift finished dimensions more than most buyers realise. Torquing – unbalanced single‑ply twist creates that ugly spiral effect. You can’t iron it out, and you can’t press it flat. We run three dynamic tests on every style: neck/cuff recovery (stretch it and see if it snaps back), light‑board scanning (every piece, no exceptions), and shade matching under D65/TL84 before linking. That last one catches dye‑lot mismatches that would otherwise only show up after packing. The five defects that actually cost you money – and how we stop them Defect What causes it Our fix on the floor Torquing / seam twist Over‑twisted yarn or uneven steam setting Pre‑knit reaming to relax twist; we slow the feed tension on the machine if the yarn feels tight; high‑temp steam set after knitting Pilling Short‑staple fibres or too much softener in the wash Switch to long‑staple/combed yarn; run a Martindale test at sample stage – if it scores below 3.5, we don’t cut Dropped stitches / holes Worn latch needles or poor linking Daily needle changes; 100% light‑board scan – zero tolerance. One hole, out of the shipment. Shading / dye‑lot variation Different dye batches or unstable vat temp Strict dye‑lot control; we hold back trims and body panels until they’re matched side‑by‑side under the lightbox Wash‑induced shrink No pre‑shrink allowance or mismatched blend rates Build 3‑5% shrink into the knitting programme; wash‑test the pilot sample and adjust before bulk Here’s a dirty little secret that doesn’t make it into the textbooks: some factories over‑stretch the rib during finishing just to hit the chest measurement on the table. That rib snaps back in transit, and suddenly your spec sheet is worthless. We check the relaxed state specifically to catch that – not the stretched number the production line wants to show you. AQL 2.5/4.0 – thresholds that actually get used We run General Inspection Level II for final random inspection. Critical defects are AQL 0 – one broken needle or a missing fibre label and the whole order stops. For a 2,000‑piece order, we pull 125 pieces. If we find 7 Majors and 10 Minors, the batch rolls. If Majors hit 8, we reject it on the spot. No debate. Real‑world classification (knits only): Major – dropped stitch, open linking seam, side‑seam twist >3%, measurement out of spec, obvious shading. Minor – loose thread >1cm inside, misplaced hang‑tag, light press mark. I’ve had third‑party inspectors flag a 2cm length difference on a heavy 5GG cable knit. We stopped the inspection, let that sweater relax flat for the full 24 hours, and re‑measured. It came back within tolerance. They signed the field report. That’s why we always build a relaxation hold into the FRI schedule – and we insist the inspector watches the re‑measure. Gauge‑specific checks: 3GG is not 12GG Coarse (3‑5GG) – gravity is your enemy. We never hang these; we measure after 24 hours flat. Linking strength gets a hard pull test at the shoulder. Mid (7‑9GG) – torquing and rib recovery are the trouble spots. We check side‑seam twist (must be ≤3%) and stretch neck/cuffs to verify snap‑back. If the rib doesn’t return, we add spandex in the next run. Fine (12‑14GG) – micro‑holes and density. 100% lightboard scan; we use a density glass to check courses and wales per inch and hold ±3% across the batch. Measurement POMs and the tolerance trap Never measure straight out of the polybag. That’s a rookie mistake that costs buyers thousands in false chargebacks. Our protocol: flat‑lay for 2‑4 hours (24 hours for coarse gauges), no stretching, non‑stretch steel tape. Core POMs we actually use: Body length – HPS to hem (including rib) Chest width – half measure, 1” below armhole Shoulder – seam to seam Sleeve length – from CB neck to cuff Neck width/depth – at seam and from back neck to front dip Tolerance sheet (by gauge): POM Fine (12‑14GG) Mid (7‑9GG) Coarse (3‑5GG) Heavy texture Body length ±1.0 cm ±1.2 cm ±1.5 cm ±2.0 cm Chest (half) ±0.8 cm ±1.0 cm ±1.5 cm ±1.5 cm Shoulder ±0.8 cm ±1.0 cm ±1.2 cm ±1.5 cm Sleeve ±1.0 cm ±1.2 cm ±1.5 cm ±2.0 cm Neck ±0.5 cm ±0.8 cm ±1.0 cm ±1.0 cm If the yarn has high spandex content, we add 0.3‑0.5cm on horizontal measures – but we flag that in the Tech Pack before production, never after the fact. Tech Pack must‑haves + handling third‑party inspectors (SGS/ITS/BV) Over 40% of disputes we mediate come down to one thing: the Tech Pack doesn’t specify the relaxed state. Yours must include: Yarn blend and count (e.g. 2/28NM) plus dye method Gauge and stitch structure, with a max float‑length limit A clear POM diagram – not just text Pantone reference and light‑source priority (D65 > TL84) Label position, thread spec, and packing details Performance numbers: pilling ≥3.5, colourfastness ≥4, shrink ≤3% For the 3rd‑party inspector: we give them a dedicated table, lightbox, and lightboard. The checklist they use must match the approved PP sample to the letter – no last‑minute tolerance changes. If they flag an out‑of‑spec measurement, our QC lead has the right to stop the process, re‑relax the piece, and re‑measure on the spot. We photograph the disputed point, sign the field report together, and keep a sealed sample for appeal. Final word (straight to the point) Knitwear quality isn’t inspected in at the end – it’s built into the yarn tension, the relaxation time, and the gauge‑specific checkpoints. If your Tech Pack doesn’t already specify the relaxed state and the recovery test, we’ve got a gap to close before we cut a single cone of yarn. If you’re sourcing knitwear and want a partner who runs these protocols daily – and who will flag the risks before they become chargebacks – send your Tech Pack over. Our technical team will give you a no‑cost feasibility read, a tolerance sample to check our finishing standards, and a supply‑chain risk review specific to your next season.
view more
How to Choose a Knitwear Manufacturer: Complete Buyer Checklist
How to Choose a Knitwear Manufacturer: Complete Buyer Checklist A Step-by-Step Sourcing Guide for Brands — Even Without a Tech Pack Sweater Manufacturer demand is rising as the global knitwear market is projected to surpass $1 trillion by 2035, with demand for high-quality sweaters continuing to grow. But for brand founders, capturing this growth isn't easy. Let’s cut the flattery. Finding a sweater factory isn’t about winning a lowball bidding war. In my experience, the cheapest quote usually comes with hidden costs: missed ship dates, inconsistent sizing, pilling after two washes, and a communication blackhole that makes you want to pull your own hair out. Smart sourcing isn’t about price. It’s about finding a manufacturing partner that’s responsive, transparent, and technically competent. Even if you don’t have a technical designer on staff or a fully built-out tech pack, you can screen factories quickly using these four core criteria. Here’s exactly how. 1. Hardware & Process: What’s Actually on the Floor Forget the glossy sales pitch. A factory’s real capability comes down to two things: the knitting machines they run and how they stitch the pieces together. Gauge (GG) Selection & Machine Capability Gauge refers to the number of needles per inch on the knitting bed. Higher GG = finer, lighter fabric. But here’s the catch: a factory needs the native machine for each gauge. You’re looking for STOLL (Germany) or SHIMA SEIKI (Japan) equipment, not knockoffs. Here’s how the gauges break down: Coarse Knit (3GG – 5GG): Heavyweight fall/winter sweaters, cable knits, cardigans. This gauge tests a factory’s tension control on wide-gauge beds. Mid-Gauge (7GG – 9GG): Your bread-and-butter spring/fall styles. This is the volume sweet spot. The key metric here is stitch uniformity across bulk production. Fine & Superfine (12GG – 18GG): Base layers, fine merino, and cashmere blends. This is where the factory’s climate control and finishing processes get scrutinized. Temperature and humidity swings wreck fine-gauge production. Red flag: A factory that claims they can run 7GG on a 12GG machine by "modifying" the settings. That’s a fancy way of saying your sweater will stretch out and lose its shape after one wear. Walk away. The Joining Process: What Determines Garment Durability This is the single biggest differentiator between a premium sweater and fast-fashion garbage. Hand-Linking (Looping): Each stitch from the knitted panels is looped onto a linking machine, one by one. The result? Seams that are flat, elastic, and almost invisible against the skin. This is how you build garments that last. Cut-and-Sew (Overlock): The cheaper, faster route. Panels get cut with scissors and stitched together with an overlock machine. The seams are bulky, have zero give, and will start fraying at the edges after a few wash cycles. Bottom line: if you’re selling a premium product, hand-linking is non-negotiable. If you’re chasing ultra-low cost, just know the trade-offs. 2. Decoding MOQ: How to Test the Waters Without Breaking the Bank Here’s a truth most brand founders learn the hard way: the MOQ bottleneck usually isn’t the factory’s knitting machines. It’s the dye house. Most mills set dye-lot minimums at 100–300 kg per color. That translates to roughly 300–1,000 finished garments, depending on weight. So how do you get started with 100–200 pieces? Stock service yarns. Stock Service vs. Custom Dyeing If you insist on a specific Pantone match, be prepared to pay for custom dyeing—and wait an extra 2–3 weeks for lab dips and strike-offs. But if you’re willing to work from the factory’s stock yarn color cards, everything changes. Criteria Stock Service Yarns Custom Dyeing MOQ Low (100–200 pcs/design) High (300–1,000+ pcs/design) Lead Time Fast (3–7 days for strike-offs) Slow (adds 2–3 weeks for color development) Risk Low—test multiple colors easily High—you’re sitting on leftover yarn Pro tip: When you send your RFQ, ask this exact question: “What’s your MOQ if we use your stock service yarns?” The answer will tell you immediately if they’re set up for agile, small-batch production or if they’re still operating in the old-school volume model. 3. Sampling Without a Tech Pack & Rigorous Quality Control A good OEM/ODM factory is essentially a development partner. They don’t need a perfect tech pack to start working with you. How to Kick Off Sampling Send them any one of these: High-res reference images or sketches—clearly mark the silhouette and pattern details you want. A physical sample garment—this is the gold standard. Even if it’s the wrong fabric or a different brand, they can reverse-engineer the measurements and build a new pattern from it. The Three Critical Samples Before Production Don’t skip these. Each one protects you from expensive mistakes. Knit-down (Yarn Swatch): This is your first sanity check. It confirms the actual yarn hand-feel, the true color, and how the stitch pattern renders. Approve this before the factory cuts a single panel. Proto Sample (First Fit Sample): This is your first look at actual garment silhouette and construction. Check the fit, the drop, the armhole depth. This is where you catch pattern issues. PPS (Pre-Production Sample): This is the non-negotiable gatekeeper. The PPS must be made with 100% production yarn, trims, and finishing processes. That means the same dye lot, the same wash, the same steam-setting. Do not—under any circumstances—authorize bulk production without a signed-off PPS in hand. The Quality Benchmarks That Matter (AQL 2.5) Hold your factory to these three metrics during the final inspection: Size tolerance: Within ±1.5 cm of the spec sheet. Pilling resistance: ISO/AATCC rating of 3–4 or higher. Anything below that and your customers will complain within weeks. Washing shrinkage: Must fall within ±3% to ±5% after the standard wash-and-set finishing process. 4. Sending a Smart RFQ & Spotting Supplier Red Flags You don’t need a novel. You need a concise, information-rich inquiry that gets you a real quote on the first pass. The Four Components of a High-Conversion RFQ Include these four elements, and you’ll get a useful response—not a generic brochure. Estimated quantity: Total pieces AND breakdown per color. (Example: 200 total, 100 pcs in Navy, 100 pcs in Charcoal) Visual reference: Either a high-quality photo or simply state: “Sample garment available for shipping.” Yarn & gauge preferences: Be specific. (Example: “7GG mid-gauge, cotton-blend, using your stock service yarns.”) Target market & delivery deadline: (Example: “US market—must hit warehouse by October 15th.”) Factory Red Flags: Three to Walk Away From I’ve seen these patterns repeat across dozens of factory audits. If you hit any of these, keep looking. Slow sampling response: If they can’t turn a proto sample around on time, they’re telling you—loudly—that they can’t manage production schedules. Bulk will be worse. Pushing custom dyeing exclusively: If they refuse to show you a stock yarn color card and insist on high-MOQ custom dyeing, they don’t have a service model for emerging brands. They’re still hunting whales. No industrial steam-setting equipment: If they’re finishing sweaters with a hand iron instead of a proper steam tunnel or press, your garments will shrink and deform after the customer’s first wash. That’s a chargeback waiting to happen. Final Take: Build a Supply Chain, Not a One-Off Deal Choosing a knitwear factory isn't a transaction. It’s the foundation of your brand’s supply chain. The playbook is simple: Use stock service yarns to de-risk your initial order. Lock down your PPS before bulk production starts. Send a tight, data-driven RFQ to filter out time-wasters. Do that, and you’ll operate like a seasoned sourcing pro—regardless of your team’s size. Ready to Skip the Sourcing Headaches? Finding a knitwear partner who balances flexible MOQs, rigid quality control, and transparent communication shouldn’t feel like a gamble. At JM Sweater (Guangzhou Junma Apparel Co., Ltd.), we’ve spent 21 years perfecting custom knitwear manufacturing for growing global brands. With a 3,000 m² facility and annual capacity of 1.2M garments, we bridge the gap between high-end craftsmanship and flexible production—whether you need low-MOQ stock yarn development or full-scale OEM/ODM runs. Need help reviewing a Tech Pack or calculating yarn yield? [Get a Free Production Assessment & Quote within 24 Hours]
view more
Italian-Standard Knitwear Manufacturing: A Technical Protocol for Premium Yarn Traceability and Factory Capability
Offshore manufacturing for Italian knitwear is governed by micro-tolerances. For European sourcing directors, the real risk is not the prototype; it is bulk execution drift. Italian knitwear is not a design aesthetic. It is fabric hand-feel, stitch tension, and micron-level craft tolerances. When partnering with an offshore sweater manufacturer, the core challenge is whether the bulk order can replicate the DNA of Italian quality—and whether raw material traceability remains absolutely transparent. True Italian manufacturing standards rest on quantifiable engineering protocols. The scope is specific: dynamic Transaction Certificate (TC) traceability for high-gauge cashmere, GRS-certified recycled yarns, and GOTS organic cotton. Tension control on 3GG–18GG fully computerized flat-knitting machines and 3D WHOLEGARMENT knitting technology. Loop-by-loop hand-linking. Mobilon tape structural reinforcement at shoulder and neck seams. Every engineering detail determines whether bulk production repeats. This guide outlines a systematic factory technical audit standard: material chain-of-custody, gauge engineering matching, structural reinforcement, and laboratory physical tolerances. It covers what brands need to execute bulk orders while safeguarding compliance and quality. Table of Contents 1. Italian Raw Material Protocol: Premium Yarn Sourcing and Chain-of-Custody (CoC) Control 2. Gauge Mechanics: Matching Italian Design with Equipment Precision (3GG to 18GG) 3. Italian Craftsmanship and Structural Integrity: Intarsia, Hand-Linking, and Structural Reinforcement 4. Bulk Repeatability: Italian Laboratory Testing and Tolerance Control Matrix 5. Enabling Italian Brands' Global Distribution: Environmental and International Trade Compliance 6. Co-Creating Italian Quality: Technical Evaluation and Free Sample Development Protocol 1. Italian Raw Material Protocol: Premium Yarn Sourcing and Chain-of-Custody (CoC) Control Italian high-end knitwear starts with precise control over natural fibers and specialty yarns. For European buyers who care about brand reputation and compliance, raw material auditing goes beyond hand-feel and yarn count. It demands rigor in the supply chain's Chain-of-Custody (CoC). Dynamic Transaction Certificate (TC) Verification for Luxury Fibers A static Scope Certificate (SC) only proves a factory holds the qualification. SC certificates mean little without batch TCs. The key to verifying actual bulk raw materials is the dynamic Transaction Certificate (TC). For high-gauge cashmere, GRS-certified recycled yarns, and GOTS organic cotton, a rigorous manufacturing system must achieve full documentation closure from spinning through dyeing to knitting. Third-party-issued batch TC certificates are required with every bulk delivery, providing 100% traceability from raw material source to finished garment. Italian Specialty Processing and Flexible Supply Chain Support (Basolan Wool and Stock Service Color Cards) For specialty fabric processing, Basolan-treated washable merino wool is used. Scale-stripping modification technology retains wool's natural soft hand-feel while significantly improving shrinkage resistance and anti-pilling performance. A Stock Service Yarn Program allows brands to directly access in-stock premium yarn counts and color palettes. This shortens sample development cycles and lowers MOQ thresholds. Italian and European brands gain small-batch, high-frequency premium rapid response. 2. Gauge Mechanics: Matching Italian Design with Equipment Precision (3GG to 18GG) Italian knitwear is known for rich texture layering and fine gauge expression, from heavyweight cable-knit cardigans to ultra-light base layers. This places extreme span requirements on equipment configuration and gauge mechanics. Full Gauge Spectrum and Yarn Count Matching Matrix Production is executed on the full 3GG to 18GG gauge spectrum using computerized flat-knitting machines. Through scientific yarn count and density matching, each garment achieves precise balance between weight, hand-feel, and structural tension: Gauge Recommended Yarn Count Typical Italian Styles Engineering Control Focus 3GG – 5GG 1.5Nm – 4.5Nm (coarse/multi-ply) Heavyweight coarse-gauge, Italian cable/aran cardigans Structural support and sag resistance 7GG – 9GG 2/28Nm – 2/48Nm (2-ply) Classic crew necks, Intarsia Fabric surface flatness and color-block separation 12GG – 14GG 2/48Nm – 2/60Nm (worsted) Business slim-fit, Basolan anti-shrink merino Gauge uniformity and wash shrinkage tolerance 16GG – 18GG 2/60Nm – 2/80Nm+ (ultra-fine) Minimalist haute couture base layers, ultra-thin cashmere Yarn tension micro-adjustment and high-gauge hand-linking Advanced Flat-Knitting Systems and 3D WHOLEGARMENT Technology (STOLL / Shima Seiki) For complex stitch structures, German STOLL and Japanese Shima Seiki flat-knitting machines are deployed. Sinker and dynamic tension control systems resolve fabric torque and surface flatness deviations that commonly occur in Italian cable knits and multi-color jacquards. European premium brands require zero waste and wearing comfort. 3D WHOLEGARMENT knitting technology addresses both. Three-dimensional integral forming eliminates traditional cut-and-sew panels and seams. The garment naturally conforms to body contours. Yarn cutting waste drops to zero. This aligns with EU circular textile directives. 3. Italian Craftsmanship and Structural Integrity: Intarsia, Hand-Linking, and Structural Reinforcement Italian knitwear quality is not only about fabric surface. It is local seam precision and structural anti-deformation engineering. Complex Pattern Structures: Intarsia vs Jacquard Pattern Engineering In large-area multi-color or geometric pattern knitting, conventional Jacquard creates floats on the reverse side. That adds fabric thickness and compromises drape. For large color-block designs, Intarsia is the specified engineering route. Independent interlocking of yarns at boundaries eliminates excess floats on the reverse. Zero floats on the reverse. Clean drape on the front. The result is a single-layer fabric surface, smooth without bulk. For complex textures requiring Jacquard, back-bed float tension and span are precisely regulated to ensure clean pattern edges and consistent lateral extensibility. Loop-by-Loop Hand-Linking and Mobilon Tape Structural Reinforcement The essence of Italian seaming is eliminating seam bulk and hard interference. Garment assembly uses loop-by-loop hand-linking. Panel edge stitches and linking machine needles align 1:1. The result: flat, high-elasticity, invisible seams with no foreign body sensation. High-gauge sweaters (14GG–18GG) lose shape quickly on hangers. To prevent this, high-quality Mobilon tape structural reinforcement is pre-embedded directly into the shoulder seams and neck collar before hand-linking. Garment appearance and soft hand-feel remain unchanged. Seams gain lasting tensile recovery. Neckline deformation and shoulder drop are resolved. 4. Bulk Repeatability: Italian Laboratory Testing and Tolerance Control Matrix The core test of premium knitwear bulk delivery is replicability from Proto to Bulk. Italian and European brands set stringent QC standards. Visual judgment is replaced by data-driven laboratory physical testing and precision tolerance control. Laboratory Physical Performance Testing Standards Bulk garments undergo rigorous physical performance testing before shipment. They must maintain Italian premium quality through daily wear and washing: Pilling Resistance: Tested per ISO 12945-2 (Martindale method) or ASTM D3512 (random tumble pilling method). Results consistently achieve Grade 3.5–4 and above. Color Fastness to Rubbing: Dry/wet crocking color fastness both achieve Grade 4. Wash Shrinkage: After standard wash-and-dry testing, fabric dimensional change in warp and weft directions remains strictly within ±3%. Spectrophotometer Dye-Lot Color Difference and Garment Tolerance Control Cross-batch dye-lot color variation and bulk pattern drift are industry pain points. Quantitative engineering control standards are applied: Dye-Lot Spectrophotometer Color Measurement: Precision spectrophotometers compare color samples. Spectrophotometer dye-lot color difference is strictly limited to ΔE < 1.0—imperceptible to the human eye. Garment Dimensional Tolerance: Ultra-narrow production tolerances are enforced. Chest width, body length, and other primary structural measurements are controlled within ±1.0 cm. Collar width, cuffs, and other detail measurements are limited to ±0.5 cm. Bulk delivery closely matches TOP Sample specifications. 5. Enabling Italian Brands' Global Distribution: Environmental and International Trade Compliance Premium Italian knitwear brands distribute across the EU, North America, and core global markets. In cross-border distribution, manufacturing compliance failures—such as unauthorized chemical residues, improper environmental labeling, or non-compliant flammability ratings—can result in customs impoundment, retail delisting, or severe regulatory penalties. Our manufacturing infrastructure embeds target-market regulatory frameworks directly into pre-production workflows and ex-factory quality assurance protocols, guaranteeing seamless international distribution for brand partners. EU and French Environmental Compliance (REACH, AGEC Law, and Triman Marking) Within EU markets, our quality control protocols enforce total chemical traceability across all yarn lots, dyeing auxiliaries, and finishing agents under REACH regulations. All incoming raw materials undergo mandatory pre-screening to verify zero Substances of Very High Concern (SVHC). To meet France's specific environmental mandates under the AGEC Law (Anti-Waste and Circular Economy Law), our production management system incorporates end-to-end material traceability and environmental impact documentation. Garments leaving the line are fitted with fully compliant French Triman markings and localized sorting instruction labels, enabling brands to pass European environmental audits effortlessly. North American Market Access Standards (FTC Care Labeling and CPSC Flammability Compliance) For export into North America, brushed, coarse-gauge, and ultra-lightweight knits require rigorous safety verification. Bulk production from our facility is routinely backed by accredited Class 1 safety testing under US CPSC 16 CFR 1610 (Standard for Flammability of Clothing Textiles). Furthermore, care labels generated during automated finishing adhere strictly to US Federal Trade Commission (FTC) 16 CFR Part 423 guidelines, featuring fully verified fiber content ratios, exact country-of-origin documentation, and standardized care instructions. This embedded compliance infrastructure eliminates regulatory bottlenecks at customs and ensures friction-free retail placement. 6. Co-Creating Italian Quality: Technical Evaluation and Free Sample Development Protocol Replicating true Italian knitwear quality never relies on verbal promises. It depends on a transparent, verifiable, data-driven factory execution system. TC transaction certificate verification for high-gauge yarns. Tension regulation on 3GG–18GG full-gauge equipment. Loop-by-loop hand-linking. Strict laboratory tolerance control. Engineered management at every stage is the fundamental guarantee for bulk quality and supply chain risk reduction. To help Italian and European brand procurement teams connect with premium manufacturing resources, our engineering team provides a responsive technical feasibility evaluation and sample development mechanism. Whether a project requires structural optimization for complex patterns (Intarsia/Jacquard) or the optimal yarn count ratio for a specific gauge, our engineering team delivers professional technical assessment and costing analysis. Start Your Tech Pack Evaluation and Free Sample Development If you are seeking a high-spec knitwear manufacturing partner capable of precisely replicating Italian craftsmanship, submit your Tech Pack or design originals. We will provide a knitting structure evaluation and engineering optimization proposal, then initiate a Free Sample Development program. This lets you verify garment fit, yarn hand-feel, and craft details at zero risk before bulk production begins, ensuring controlled execution of subsequent volume orders.
view more